Microcrystalline Cellulose Bulk Density and Particle Size: Troubleshooting Tablet Weight Variation
Quick answer: Microcrystalline cellulose bulk density and particle-size distribution influence hopper flow, die filling, blend uniformity, tablet weight variation, compactability and press output. When tablet weight becomes unstable, do not change compression force first. Confirm the actual MCC lot profile, compare it with the approved baseline, check segregation risk in the complete blend, and reproduce the problem at realistic feed-frame speed. A useful investigation connects material data to the point where powder enters each die.
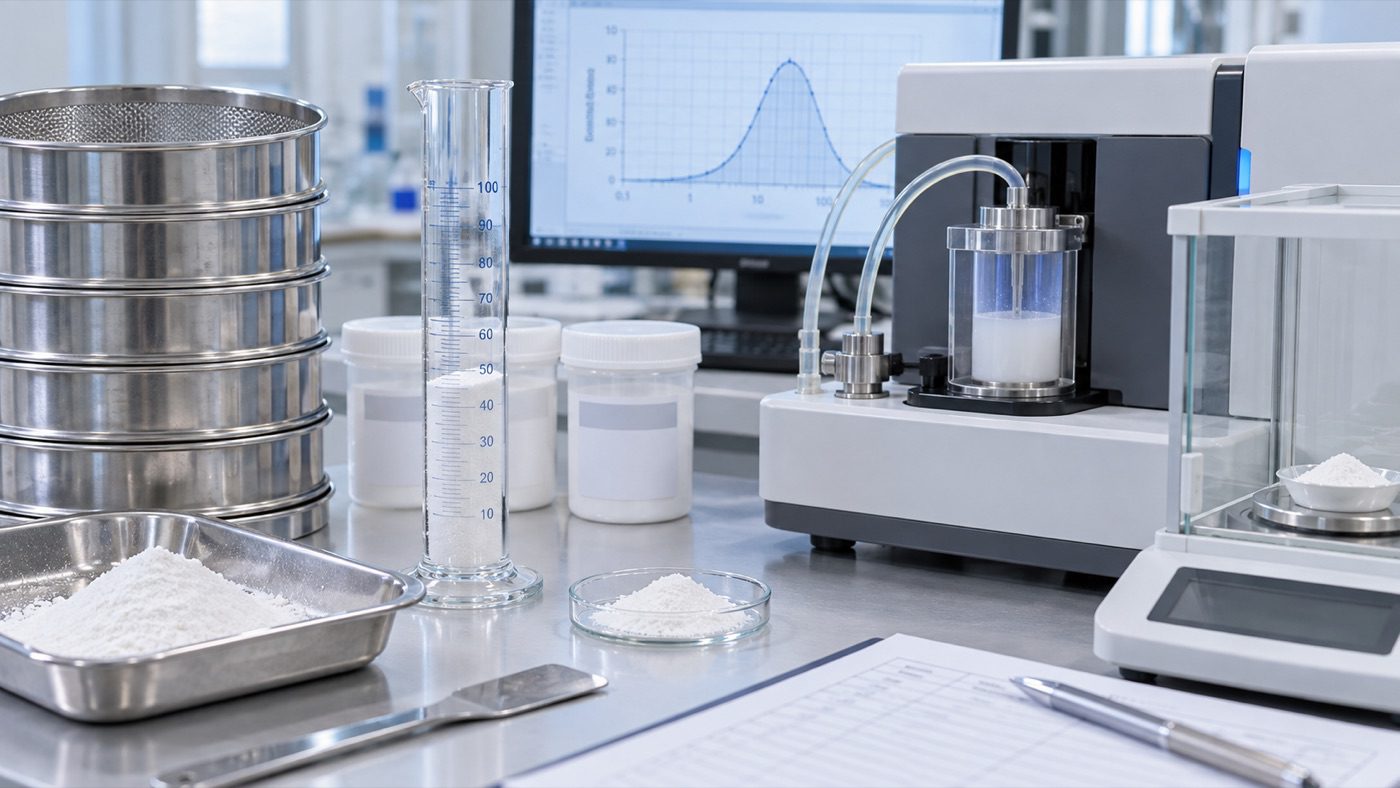
Tablet weight variation is often described as a machine problem, but the press can only meter the powder delivered to it. A formulation that flows inconsistently, aerates, segregates or changes density inside the hopper will produce an unstable die fill even when tooling and controls are in good condition. Microcrystalline cellulose (MCC) is widely used as a filler-binder because it combines dilution capacity, plastic deformation, compactability and disintegration support. Those benefits do not mean every MCC grade or lot behaves identically.
This guide explains how microcrystalline cellulose bulk density and particle size should be interpreted, tested and linked to tablet performance. It is written for formulation scientists, production engineers, quality teams and buyers who need a practical troubleshooting method rather than a generic grade description. For a broader supplier approval framework, see our microcrystalline cellulose supplier qualification guide.
Why bulk density and particle size matter together
Bulk density expresses the mass of an unsettled powder divided by the volume it occupies under a defined test procedure. Particle-size distribution describes the proportions of fine, intermediate and coarse particles. The two properties are related to powder structure, but they are not interchangeable. Two MCC samples can have a similar average particle size and different bulk densities because morphology, porosity, moisture, fibrillation and processing history differ. Two samples can also have similar bulk density while their fine fraction and upper particle-size tail are materially different.
In direct compression, these attributes affect several operations at the same time. A lower-density powder occupies more volume for the same mass, changes blender fill level and can require a deeper die fill. A coarser grade may flow more easily through the hopper, yet it may segregate from a fine active pharmaceutical ingredient. A fine MCC grade can provide high compactability and mixing contact, but it may flow slowly or retain more air. The correct choice is therefore a formulation match, not a universal maximum or minimum.
Current supplier literature illustrates the practical range. Roquette reports MCC grades with different mean particle sizes and bulk densities, while JRS Pharma describes medium, high-density and coarse grades for different flow and compression needs. These published values are useful orientation, not a substitute for the buyer’s own approved specification and compression trial. Review the technical context in the Roquette MCC troubleshooting resource and the JRS Pharma MCC grade overview.
What microcrystalline cellulose bulk density actually tells you
Bulk density is frequently treated as a warehouse number, but it has direct process implications. It changes the volume occupied by a batch, the available blender headspace, the depth of material over the feeder, the die volume needed for a target tablet weight and the apparent response to vibration. When a replacement MCC lot has a lower bulk density than the established material, the same tablet mass needs a larger volume. A press that is already near its maximum fill depth may then show underweight tablets or require a different dosing setting.
Higher bulk density can improve volumetric throughput and sometimes supports steadier feeding, especially with high-density actives. However, it does not automatically guarantee better tabletability. The densification route can change accessible surface, pore structure and deformation behavior. A grade selected only because it flows through a funnel may produce weaker compacts, different disintegration or altered lubricant sensitivity. The correct test links density to flow, filling and mechanical properties.
Bulk density versus tapped density
Tapped density is measured after a defined tapping procedure that allows the powder bed to consolidate. Comparing bulk and tapped density gives useful indicators such as the Hausner ratio and Carr index. A large difference suggests that the powder can rearrange substantially under vibration or handling. That may matter when an MCC blend travels from an intermediate bulk container through a transfer line, hopper and feed frame before compression.
These indices are screening tools. They should not be used as stand-alone release criteria unless their relationship to the formulation and process has been demonstrated. Some cohesive powders do not flow through a simple funnel but are handled adequately by an assisted feeder. Other blends look acceptable in a static test and segregate under production vibration. Always combine compendial-style measurements with a process-relevant dynamic assessment.
Why the test method must be controlled
Density results are sensitive to sample conditioning, container geometry, filling technique, vibration, leveling, temperature and moisture. Pouring a sample rapidly can trap more air than transferring it through a standardized funnel. Shaking or tapping the cylinder before the initial reading destroys the meaning of bulk density. A good laboratory procedure defines sample mass, vessel volume, transfer method, settling time and calculation. It also identifies whether the reported result is loos bulk density, poured density, aerated density or another condition.
During a supplier comparison, use the same method for all samples. Record the supplier’s method separately and avoid assuming that numbers from different technical data sheets are directly comparable. If the supplier certificate shows a value outside the customer’s historical range, first check method alignment before declaring a material shift.
Particle-size distribution: look beyond the average
An average particle size can hide the part of the distribution causing the problem. For laser diffraction, D10, D50 and D90 provide a more useful picture: approximately 10%, 50% and 90% of the measured particle volume fall below the respective diameter. Sieve results provide retained fractions at specified mesh sizes. The methods describe particles differently, so values should not be mixed without correlation.
The fine fraction is important because fines can increase cohesion, dusting, electrostatic behavior and air retention. Fines may also improve contact with a low-dose active and reduce certain segregation mechanisms. The coarse tail may support gravity flow but can create size-driven segregation if the other formulation components are much finer. A broad distribution may pack efficiently, yet it can respond differently to vibration than a narrow distribution.
Particle shape and porosity are hidden variables
MCC particles are porous and irregular rather than ideal spheres. Aspect ratio, surface roughness and internal pore structure influence friction, liquid uptake and compaction. Laser diffraction often reports an equivalent spherical diameter, which is useful for lot comparison but does not fully describe morphology. Microscopy can help when two samples have similar D50 values but unexpectedly different flow or compactability.
Moisture also changes particle interactions. Water associated with cellulose can influence plasticity, hydrogen bonding and electrostatic behavior. Therefore, a particle-size investigation should include loss on drying or an appropriate water determination. If a material was sampled immediately after a cold shipment and tested before equilibration, condensation or temperature differences can distort the comparison.
How MCC properties create tablet weight variation
Rotary tablet presses fill dies in a very short time. The powder must move from the hopper into the feed frame, remain sufficiently uniform as paddles distribute it, and enter each die consistently. Weight variation occurs when the mass delivered during that interval changes from die to die or over time. Several MCC-related mechanisms can produce the same symptom.
1. Inconsistent gravity flow
A cohesive blend may form stable arches, intermittent channels or zones of different packing density in the hopper. The feed frame receives material in pulses. The tablet weights can oscillate, drift after a refill, or become more variable as the hopper level falls. Coarser or higher-density MCC may improve the situation, but formulation segregation must be checked before changing grade.
2. Aeration and density change
Pneumatic transfer, long drops and vigorous blending can entrain air. An aerated MCC-rich blend initially occupies more volume and may settle during the compression run. If fill depth remains constant while apparent density rises, tablet weight can trend upward. The pattern may be misinterpreted as a press-control fault. Compare the beginning, middle and end of the run and record the time after transfer.
3. Segregation by size or density
A coarse MCC blended with a fine, dense active can separate during discharge and vibration. Tablet weight may remain acceptable while content uniformity changes, or both can shift if the segregated fractions have different bulk densities. Sampling only the blender can miss segregation introduced by the transfer path. Samples should represent the feed container, hopper and compressed tablets across time.
4. Feed-frame overworking
High paddle speed can densify or de-aerate the blend inside the feed frame. It can also cause attrition, lubricant redistribution or recirculation. MCC is a plastically deforming material and is sensitive to lubrication conditions. When the feeder is run much faster than necessary, the mass in the dies may stabilize while tablet hardness falls. A troubleshooting trial should vary feeder speed independently from turret speed where the equipment allows it.
5. Poor match between die volume and material density
If the formulation needs nearly the full available fill depth, a lower-density MCC lot can remove the process margin. Underweight tablets then appear first at higher press speeds or with shallow tooling. Conversely, changing to a denser grade without reformulation can increase tablet weight at the existing setting and alter the compaction profile. Confirm the relationship among target mass, blend density, fill depth and tooling capacity.
A step-by-step troubleshooting workflow
Step 1: define the failure pattern
Collect time-resolved tablet weights rather than only a final average and relative standard deviation. Determine whether the variation is random, cyclical, associated with hopper refills, progressive from start to finish, limited to particular stations or triggered by a speed increase. Map the event against feeder speed, turret speed, fill depth, compression force, hopper level and environmental conditions.
A station-specific pattern points toward tooling or mechanical causes. A process-wide drift that follows hopper level or transfer time points more strongly toward powder behavior. This distinction prevents unnecessary material changes.
Step 2: verify the material identity and lot history
Confirm the MCC grade, manufacturer, site, lot, retest date, packaging integrity and storage conditions. Compare the certificate with the approved specification and historical lot data. Check bulk density, tapped density, particle-size distribution, moisture and any functionality-related characteristics included in the agreement. Do not limit the review to compendial identity and purity tests.
Step 3: resample correctly
Powder can segregate inside a bag or drum during transport. A single top sample may not represent the lot. Use a justified sampling plan and avoid a thief method that selectively captures fines or coarse particles. Where permitted, compare top, middle and lower locations and composite according to the procedure. Protect the sample from humidity exchange.
Step 4: repeat physical characterization
Measure bulk density, tapped density, PSD, moisture and flow using controlled methods. Add angle of repose, flow through an orifice, shear-cell testing or dynamic powder testing where these tools are relevant. Examine morphology if the routine tests cannot explain the shift. Run both the suspect lot and a retained good lot in the same session to reduce method-to-method variation.
Step 5: test the complete blend
MCC data alone do not predict the behavior of the formulation. Prepare matched blends using the same raw-material lots, order of addition, blender loading, speed and mixing time. Control lubricant addition carefully. Compare bulk and tapped density, flow, PSD where appropriate, moisture and segregation tendency. A formulation with a wide density or size mismatch among components deserves special attention.
Step 6: reproduce realistic compression conditions
A slow single-punch test may show good tablet hardness while hiding a high-speed filling problem. Use a rotary press, instrumented press or compaction simulator that can approximate production dwell time and feeder conditions. Evaluate several press speeds and feeder settings. Record weight, hardness or tensile strength, thickness, friability, disintegration, ejection behavior and visible defects.
Step 7: change one factor at a time
Useful experiments include controlled changes to feeder speed, hopper agitation, transfer method, blend hold time, press speed and fill depth. If comparing MCC grades, keep the rest of the formulation constant and adjust settings only through a predefined protocol. Simultaneous changes can produce an apparently successful batch without identifying the real cause.
Interpreting common investigation results
| Observed result | Likely interpretation | Next check |
|---|---|---|
| Weight rises gradually after transfer | Aerated blend is settling and increasing apparent density | Compare density versus hold time and reduce drop height or transfer energy |
| Variation increases as hopper empties | Head pressure, bridging or segregation may be changing feed | Map hopper level, inspect flow pattern and sample by run interval |
| Coarse MCC improves weight but worsens assay uniformity | Flow improved but API segregation increased | Compare component PSD and density; review premixing strategy |
| High feeder speed stabilizes weight but reduces hardness | Feed-frame work or lubricant redistribution may be affecting compactability | Optimize paddle speed and magnesium stearate exposure |
| Supplier COA passes but press behavior changes | Release limits may be too broad or omit a functional attribute | Trend internal data and establish a performance-linked range |
| Only specific stations are unstable | Tooling or mechanical condition is more likely than MCC | Inspect punches, dies, cams, dosing and weight-control feedback |
Grade selection: fine, standard, coarse or high density?
A fine MCC grade is often considered when compactability, wet granulation, dry granulation or close mixing with fine ingredients is important. It may have less favorable gravity flow. A standard direct-compression grade commonly balances flow and compactability. Coarse grades can support high-speed filling and reduce weight variation in suitable formulations, but the risk of segregation should be assessed. High-density grades can be useful with dense actives or when volumetric capacity is limited.
Low-moisture grades address a different variable. They may be preferred for moisture-sensitive ingredients, yet low water content can change compactability and static behavior. The lowest moisture value is not automatically the best choice. Evaluate the actual active, process and packaging. Our MCC 101 versus 102 selection guide provides a starting comparison, but commercial names should always be translated into measurable attributes and confirmed by trial.
Building a performance-linked MCC specification
A compendial monograph establishes essential quality requirements, but a direct-compression application may need additional controls. A buyer can define internal alert ranges for bulk density, tapped density, selected PSD points and moisture, supported by development and manufacturing data. These ranges should not be copied blindly from another formulation. They must reflect the product’s design space and the capability of qualified suppliers.
Start by plotting lot results against tablet outcomes. Include press speed, fill depth, weight RSD, tensile strength, friability and disintegration. Look for trends rather than waiting for a formal failure. If tablets remain robust across a broad material range, avoid an unnecessarily tight specification that creates supply risk. If small changes consistently affect die fill, negotiate a narrower functional range or qualify a more suitable grade.
A certificate of analysis is most useful when methods are aligned and values are reported numerically. “Conforms” gives less information for trending. The quality agreement should cover test methods, sampling, change notification, atypical results, deviation communication, retest policy and access to supporting data. IPEC’s excipient qualification resources provide a useful framework for supplier and user responsibilities; see the IPEC excipient qualification guide overview.
Incoming quality control and lot trending
For an established product, incoming tests should be proportional to risk and supported by supplier qualification. Identity and compendial tests remain fundamental. Functionality testing can include density, PSD and moisture when they are linked to critical process performance. A fast internal screen may be used at receipt, while a more detailed method supports investigation and periodic verification.
Trend data by supplier, manufacturing site, grade and lot. Record the laboratory method version and relevant conditioning. Use control charts or simple run charts to detect shifts within specification. A gradual movement toward the limit can warn of a process change before it causes a compression deviation. When a shift appears, ask the supplier whether raw-material source, hydrolysis, washing, drying, milling, blending or packaging conditions changed.
Scale-up and technology-transfer considerations
Scale-up changes more than batch size. Blender geometry, fill level, discharge pattern, transfer distance, hopper residence time, feeder design and tablet-press dwell time can all change. An MCC grade that performs well on a laboratory press may show different weight control at commercial speed. Development trials should challenge the expected range of material attributes and use press conditions that approximate production.
During technology transfer, send the receiving site a material profile rather than only the grade name. Include the approved manufacturer and site, density and PSD history, moisture range, blend procedure, hold-time limits, transfer method, target feeder settings and known failure modes. This information reduces the temptation to solve a material-flow problem by increasing compression force.
Procurement questions that prevent future deviations
- Which manufacturing site and production route supply the offered MCC grade?
- What are the typical and release ranges for bulk density, tapped density, PSD and moisture?
- Which methods are used, and can the supplier provide method details for correlation?
- Are results reported numerically on each certificate of analysis?
- Can samples from three representative commercial lots be supplied?
- How are lots blended or standardized to control physical properties?
- Which changes require advance customer notification?
- What are the packaging barrier, palletization, storage and transport conditions?
- Can the supplier support a compression trial and investigation with technical data?
- What are lead time, minimum order, safety-stock options and supply continuity plans?
Price should be evaluated as total process cost. A small unit-price saving can disappear after slower press speed, additional testing, weight rejects, content-uniformity risk or production downtime. A technically responsive supplier helps the customer define a robust material profile and supports change control after approval.
Method precision and measurement-system checks
Before tightening a specification, confirm that the measurement system can distinguish meaningful material differences from laboratory noise. Density and sieve tests can be strongly operator-dependent when pouring speed, leveling, tapping, cleaning or endpoint decisions are not standardized. Laser diffraction results can shift with dispersion pressure, refractive-index settings, obscuration and data model. A difference between laboratories is not automatically a difference between MCC lots.
Use replicate measurements, multiple analysts and representative days to estimate repeatability and reproducibility. Include a retained reference material when practical. If the analytical variation consumes a large part of the proposed acceptance range, improve the method before using it for supplier decisions. Method transfer should document equipment configuration, sample preparation, environmental conditioning, calculation and rounding. Photographs or short controlled demonstrations can clarify physical handling steps that are difficult to communicate in a written procedure.
For troubleshooting, retain the original result and all raw observations. Do not repeatedly retest until an acceptable number appears. Atypical but in-specification results can be valuable early signals. Review them with manufacturing performance, shipment history and supplier trend data. The goal is to understand whether the result represents the lot, the sample or the measurement process.
Designing a robust three-lot compression study
A supplier qualification trial should normally include more than one hand-selected sample. Request three representative commercial lots produced across meaningful time intervals when possible. Include a retained approved lot as a control. Condition all materials consistently, prepare matched blends and randomize the run order so that equipment warming, room humidity or operator learning does not favor one sample.
Challenge more than the nominal press setting. Evaluate a low, target and high production speed, together with justified feeder settings. Measure tablet weight at frequent intervals and retain the individual values, not only the summary. Record tensile strength or hardness, thickness, friability, disintegration, ejection force, visual defects and content uniformity where relevant. Take blend or tablet samples at the beginning, middle and end to detect time-dependent segregation.
The acceptance rule should be written before the trial. It may combine specification compliance, no meaningful trend in tablet weight, acceptable mechanical strength, no adverse effect on disintegration and no new operating intervention. A supplier should not be approved solely because one optimized run passed after multiple undocumented adjustments. The approved operating window and the material profile should be captured together.
Packaging, transport and warehouse effects
MCC can arrive within specification and still behave differently if packaging or handling changes. Bag compression on pallets, repeated vibration, long sea transit, temperature cycling and warehouse humidity can redistribute fines or change powder-bed packing. Inner-liner integrity and closure quality matter because cellulose interacts with environmental moisture. Pallet height and stacking pressure can also affect the degree of compaction inside lower bags.
During an investigation, compare damaged and intact packages, pallet positions and arrival conditions. Allow cold material to equilibrate while still sealed before opening to avoid condensation. Define warehouse sampling and bag-handling practices that do not create additional segregation. If performance differs by package location, involve the supplier and logistics provider rather than adjusting the tablet press around an uncontrolled transport effect.
Frequently asked questions
Does higher MCC bulk density always reduce tablet weight variation?
No. Higher density can increase the mass delivered for a given die volume and may improve volumetric efficiency, but weight variation also depends on flow consistency, aeration, feeder action, segregation, tooling and control settings. Confirm the full blend response on the intended press.
Is D50 enough to compare two microcrystalline cellulose grades?
No. D50 describes the middle of a distribution but does not show the fine fraction, coarse tail, shape, porosity or moisture. Compare D10, D50, D90 or justified sieve fractions, plus bulk density and relevant performance results.
Can a passing certificate of analysis guarantee direct-compression performance?
No. The certificate confirms results against agreed tests and limits. It cannot reproduce the customer’s formulation, transfer path, feeder and press speed. Supplier data, incoming controls and process-relevant qualification trials are complementary.
Why can tablet hardness fall when weight variation improves?
A faster feed frame may make die filling more consistent while increasing shear, residence time or lubricant redistribution. MCC is sensitive to lubrication and processing history. Optimize weight control and mechanical strength together.
When should an MCC lot trigger additional testing?
Additional review is appropriate after a trend shift, transport excursion, damaged packaging, atypical density or PSD, unexplained press behavior, supplier change notification, complaint or significant process deviation. The decision should follow the product’s risk assessment and quality system.
What information should be included in an MCC inquiry?
Provide the dosage form, manufacturing route, tablet weight, press speed, active loading, current grade, critical density and PSD targets, moisture sensitivity, annual demand, required standards, destination market, documentation list, sample quantity and trial schedule.
Final troubleshooting checklist
- Define whether the variation is random, cyclical, progressive or station-specific.
- Confirm MCC identity, lot, manufacturer, site, storage and transport history.
- Compare bulk density, tapped density, PSD and moisture with a retained good lot.
- Verify method equivalence before comparing supplier and customer results.
- Characterize the complete blend and assess aeration and segregation.
- Reproduce the issue at realistic turret and feeder speeds.
- Separate material, formulation and mechanical hypotheses.
- Change one variable at a time and record the response.
- Link material trends to tablet weight, strength, friability and disintegration.
- Update the control strategy, supplier agreement or grade selection based on evidence.
Request a technically matched MCC sample and quotation
Hengyi Technology supports buyers evaluating microcrystalline cellulose for direct compression, granulation, tablets, nutritional products and related solid formulations. To receive a relevant recommendation, send your present MCC grade, target particle-size profile, bulk-density range, dosage form, press speed, annual quantity, destination country and required documentation.