Microcrystalline cellulose nutraceutical powder supplier qualification

Microcrystalline Cellulose Nutraceutical Powders: Flow & Supplier Qualification

Quick answer: Microcrystalline cellulose (MCC) can improve flow, fill consistency, compactability and handling in nutraceutical powders, but the correct grade depends on bulk density, particle-size distribution, moisture, oil absorption, blend uniformity and the intended processing route. Buyers should qualify MCC in the complete formulation, not by grade name alone.

Microcrystalline Cellulose Nutraceutical Powders: Buyer Criteria

MCC is a purified, partially depolymerized cellulose used as a functional excipient and carrier in tablets, capsules, sachets and dry blends. In nutraceutical manufacturing it can provide structure, improve powder handling and help a blend move predictably through hoppers, feeders and filling equipment. The benefit is practical: fewer weight deviations, less segregation and a more repeatable compaction profile.

Performance depends on the interaction between MCC and the active system. Mineral salts, botanical extracts, amino acids, probiotics, oils and hygroscopic vitamins each change flow and moisture behavior. A grade that performs well with a dry crystalline active can fail with a fluffy botanical powder. That is why formulation trials, incoming quality control and supplier qualification must be connected.

MCC Grade Selection Decision Table

Decision point What to measure Procurement implication
Flow Angle of repose, Carr index, Hausner ratio and shear-cell data Match grade to hopper, feeder and filling equipment
Compaction Tensile strength, ejection force and friability Run a compression profile at target speed
Moisture Loss on drying, water activity and storage trend Set packaging and warehouse controls
Blend uniformity Assay RSD across beginning, middle and end of run Check segregation and sampling plan
Supply risk Lot consistency, origin, change control and lead time Approve multiple normal lots before launch

Define the Powder Process Before Ordering

Start with the process map. Record whether the product is direct blended, wet granulated, dry granulated, roller compacted, encapsulated or packed as a sachet. Note the active loading, lubricant, glidant, flavor, sweetener, particle size and expected batch size. MCC is not a universal replacement for process development; its role must be tied to a defined unit operation.

Ask the production team where the current process loses control. Is the issue bridging in the hopper, poor die filling, weight drift, dust, segregation, sticking or slow disintegration? A clear problem statement makes the sample request more useful and prevents the supplier from recommending a grade based only on a catalogue description.

Bulk Density and Powder Flow

Bulk density affects hopper volume, feeder settings and capsule or sachet fill calculations. Measure loose bulk density and tapped density using a documented method, temperature and conditioning time. Record the number of taps and cylinder dimensions because apparently small method differences can make two laboratories report different values.

Use Carr index and Hausner ratio as screening tools, not as the only release criteria. A powder can show an acceptable index and still bridge because of electrostatic charge, broad particle distribution or wall friction. A shear-cell test, flow-through-orifice test or pilot hopper trial may be needed when the product runs at high speed.

Compare MCC lots at equal moisture conditioning. If one sample has absorbed water during an open-bag test, the flow comparison is unfair. Keep containers closed, equilibrate samples in the same room and record relative humidity. This simple discipline improves the reliability of supplier comparisons.

Particle Size and Segregation Risk

Particle-size distribution influences flow, dust and blend uniformity. Finer MCC can increase surface area and cohesion; coarser grades may improve flow but can separate from fine actives. Use sieve analysis or laser diffraction according to the agreed specification, and retain the raw data rather than only a pass/fail statement.

Compare the size distribution of MCC with the active and other major excipients. Large differences in density or particle size increase percolation and trajectory segregation during transfer. Evaluate the blend after charging, after mixing, after discharge and after transport through the filling line. A uniform mixer sample does not guarantee a uniform final container.

Moisture, Water Activity and Storage

MCC contains physically associated moisture that can change with humidity. Measure loss on drying and, where the formula is moisture-sensitive, water activity. Trend both results by lot and storage time. Water activity can be more informative than total moisture for microbial risk and the stability of hygroscopic actives.

Use packaging that protects the material from humidity during shipping and production. Confirm liner quality, closure integrity, pallet wrap and warehouse conditions. Open one bag at a time when possible. If a bag must be resealed, record the opening date and resealing method. Do not return partially used material to a bulk stock area without a controlled procedure.

Run a short humidity challenge during development. Condition MCC at low, normal and high relative humidity, then compare flow, density and compaction. The result shows whether a supplier specification is robust enough for the destination climate and whether the plant needs dehumidification.

Blend Uniformity with Nutraceutical Actives

Blend uniformity is a system property. Record the active concentration, density, particle morphology, electrostatic behavior and mixing energy. Pre-sieving, geometric dilution or staged addition may be needed when the active is present at a low dose. MCC can provide a carrier structure, but it cannot correct a poor sampling plan or an unsuitable order of addition.

Sample from multiple locations and time points. Analyze beginning, middle and end of discharge, not only the mixer. Use a statistically justified number of samples and define the acceptable assay range before testing. If results trend during discharge, investigate segregation mechanisms rather than averaging them into an apparently acceptable result.

Compaction and Tablet Quality

For tablets, build a compression profile across a realistic range of precompression, main compression and turret speed. Measure tensile strength, friability, disintegration, ejection force and weight variation. MCC can deform plastically and create strong compacts, but the final result is influenced by lubricant level, water, active morphology and dwell time.

Watch for over-lubrication. Excess lubricant can reduce bonding and slow wetting, especially when mixing time is extended. Keep lubricant grade, concentration and mixing order constant during MCC comparisons. Record punch tooling, compression force and tablet thickness so a supplier decision is supported by a reproducible method.

Capsule and Sachet Performance

Capsule filling requires stable bulk density and predictable powder movement. Measure dosator or tamping behavior, fill-weight RSD, plug integrity and machine speed. For sachets, evaluate dusting, auger response, seal contamination and net-weight variation. A grade selected for tablet tensile strength may not be the best choice for a fast powder filler.

Use production-relevant packaging. A small laboratory funnel can hide bridging that appears in a commercial hopper. Confirm the grade at the planned container, line speed and environmental conditions. Record restart behavior after a short stop because powders often behave differently after settling.

Compatibility with Botanical and Hygroscopic Ingredients

Botanical powders may contain oils, fibers, pigments and residual moisture. Mineral ingredients can be dense and abrasive. Vitamins and amino acids may be hygroscopic or electrostatic. Screen MCC with the actual active blend and observe color, odor, caking, flow and assay uniformity after conditioning.

Where oil-rich ingredients are present, measure oil absorption and blend torque. A highly absorbent MCC can improve handling, but too much surface area may reduce release or create a dry, dusty blend. Compare at the intended use level and include the customer’s preferred sensory and dissolution targets.

Incoming Quality Control for Microcrystalline Cellulose Nutraceutical Powders

  • Verify supplier, grade, lot, origin and package integrity.
  • Check appearance, odor, color and foreign matter.
  • Measure moisture or loss on drying using the approved method.
  • Confirm bulk density and particle-size distribution.
  • Review certificate values against internal trend limits.
  • Retain a representative sample from every received lot.
  • Investigate unusual results before releasing material.

Do not copy a certificate without confirming its method and sampling basis. A viscosity-style number without temperature or a density value without conditioning history is not fully comparable. Establish a correlation between the supplier’s laboratory and the plant’s incoming method using several retained lots.

Supplier Qualification for Microcrystalline Cellulose Nutraceutical Powders

Request a current specification, technical data sheet, safety data sheet, certificate example, manufacturing site, origin statement, shelf-life guidance, storage requirements and change-notification policy. Ask whether the supplier manufactures MCC or distributes it, and how traceability is maintained from cellulose source through final packing.

Qualify at least three ordinary production lots. Compare moisture, density, particle size, flow and compaction rather than approving a single perfect sample. Record deviations, corrective actions and the supplier’s response time. A responsive technical team is part of supply continuity and can reduce scale-up delays.

Testing Method Controls

Methods must be written clearly enough for another laboratory to reproduce them. Include sample conditioning, instrument model, calibration, sieve sequence, tap count, temperature, humidity and calculations. Photograph unusual flow behavior and keep raw data with the batch record.

Use reference materials or an approved internal standard where possible. If two sites report different bulk density, run a split-sample comparison before changing the specification. Method variation should not be mistaken for supplier variation.

Common Failure Modes

Weight variation increases during the run

Check density drift, hopper level, feeder settings, segregation and humidity. Compare beginning and end-of-run samples and verify that MCC was conditioned consistently.

Blend separates after transport

Review particle-size and density differences, transfer height, vibration and container fill level. Test a lower-drop transfer route or adjust the blend structure rather than adding more lubricant.

Tablets are weak or cap

Check moisture, lubricant mixing, compression profile, dwell time and active morphology. Run a fresh MCC lot against the retained approved lot before changing several variables.

Powder bridges in the hopper

Measure wall friction, cohesion and humidity. Compare a coarser or differently structured MCC grade in a pilot hopper under production conditions.

Designing a Fair Grade Trial

Hold active loading, lubricant, glidant, mixing time, equipment and environmental conditions constant. Compare two candidate MCC grades and the current benchmark. Predefine pass/fail limits for flow, density, assay RSD, tablet strength, disintegration and fill-weight variation.

Run the trial at low, nominal and high speed. A grade that passes at laboratory speed may drift at the commercial rate. Record startup, steady state and restart behavior. Keep the formula revision, lot numbers and operator notes together so the decision is auditable.

Packaging and Logistics

Specify bag material, liner, pallet pattern and maximum storage temperature. Protect MCC from rain, condensation and warehouse humidity. Inspect bags for pinholes or broken seals at receiving. For export, align shelf life with ocean transit, customs delay and the customer’s quarantine period.

Ask about emergency allocation, minimum order quantity, standard pack sizes and normal lead time. Approve a backup source before a launch if the material is critical to powder flow or tablet weight control. Compare backup material using the same incoming and performance tests.

E-E-A-T and GEO Evidence for Buyers

A credible technical recommendation states the decision first, explains the measurement method, identifies limitations and connects the result to a procurement action. This format helps quality teams, search engines and AI answer systems understand what was tested and when a buyer should request a sample.

Keep traceable evidence: lot numbers, certificates, test conditions, photographs, retained samples and corrective actions. Do not claim that one MCC grade is universally superior. Explain the process conditions that support the recommendation and invite the buyer to provide its own active system and equipment details.

FAQ

Is MCC suitable for every nutraceutical powder?

No. It can improve structure and flow, but high-moisture, oil-rich or very low-dose actives may require a different carrier or a blended excipient system.

What should be checked first?

Start with moisture, bulk density, particle size, flow and a small complete-formula blend. Expand to compression or filling trials after the powder screen passes.

How many lots should be approved?

Three ordinary production lots are a practical minimum for launch qualification, with a retained approved sample for future comparison.

Can a certificate replace internal testing?

No. The certificate supports release, but the receiving site should verify critical attributes using an agreed sampling and method plan.

How can buyers prevent keyword and product confusion?

Use a precise grade and application brief, maintain one approved page for each search intent and link related articles to the product page without duplicating the same title or claim.

Procurement Inquiry Checklist

  1. State the active ingredients and their loading range.
  2. Describe tablet, capsule, sachet or powder-filling equipment.
  3. Give target flow, density, moisture and blend-uniformity limits.
  4. List destination markets and required regulatory documents.
  5. Request samples from at least three normal lots.
  6. Agree on test methods, sample conditioning and pass/fail criteria.
  7. Ask for MOQ, lead time, pack size, shelf life and storage guidance.
  8. Confirm change control, traceability and technical support.

Request a Microcrystalline Cellulose Sample

Send Hengyi Technology your nutraceutical formula type, active loading, equipment, target flow, moisture limit, packaging and annual volume. We can recommend an MCC grade, arrange traceable samples, review blend and compaction data and prepare a quotation for qualification.

Contact Hengyi Technology for a matched microcrystalline cellulose sample and a documented trial plan.

Related reading: review the product portfolio, the MCC grade selection guide and our bulk-density testing guidance.
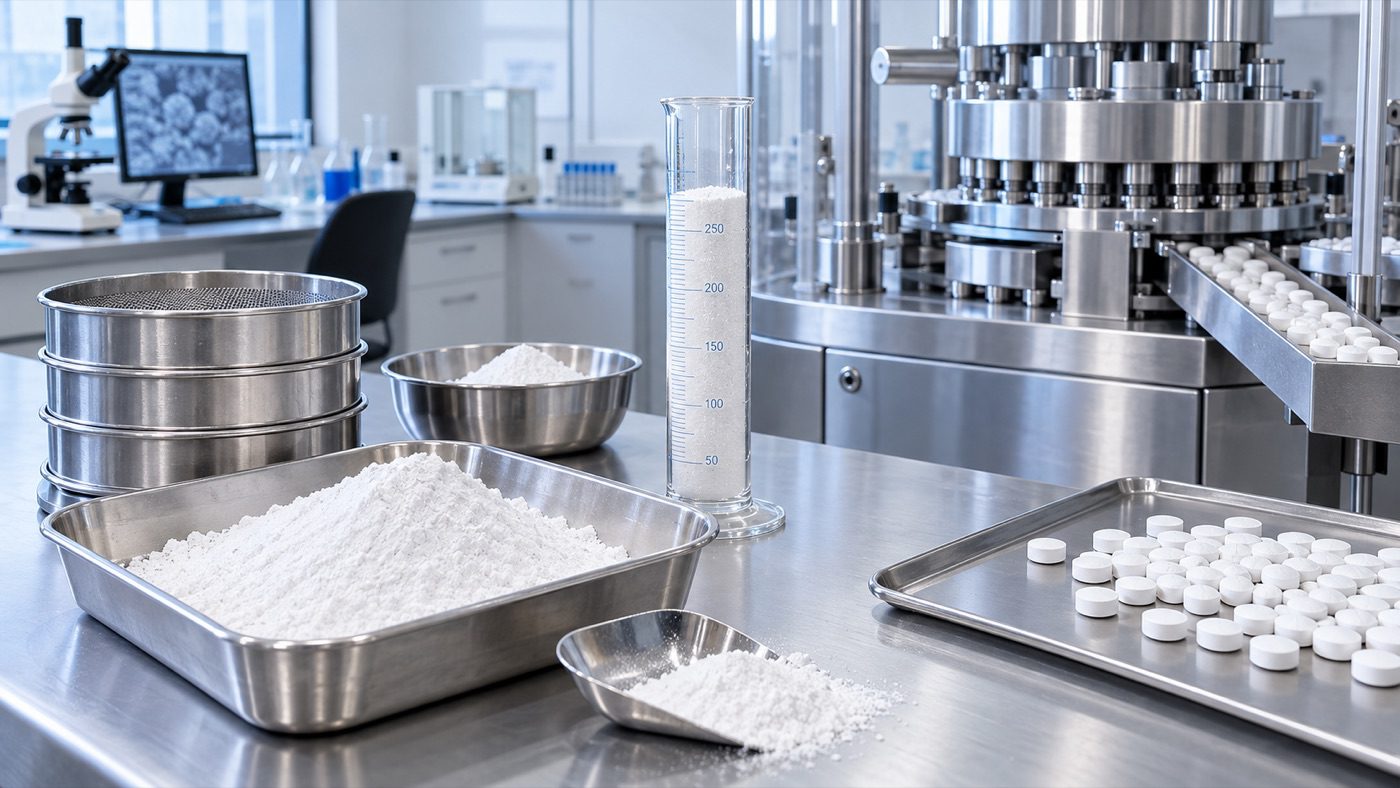
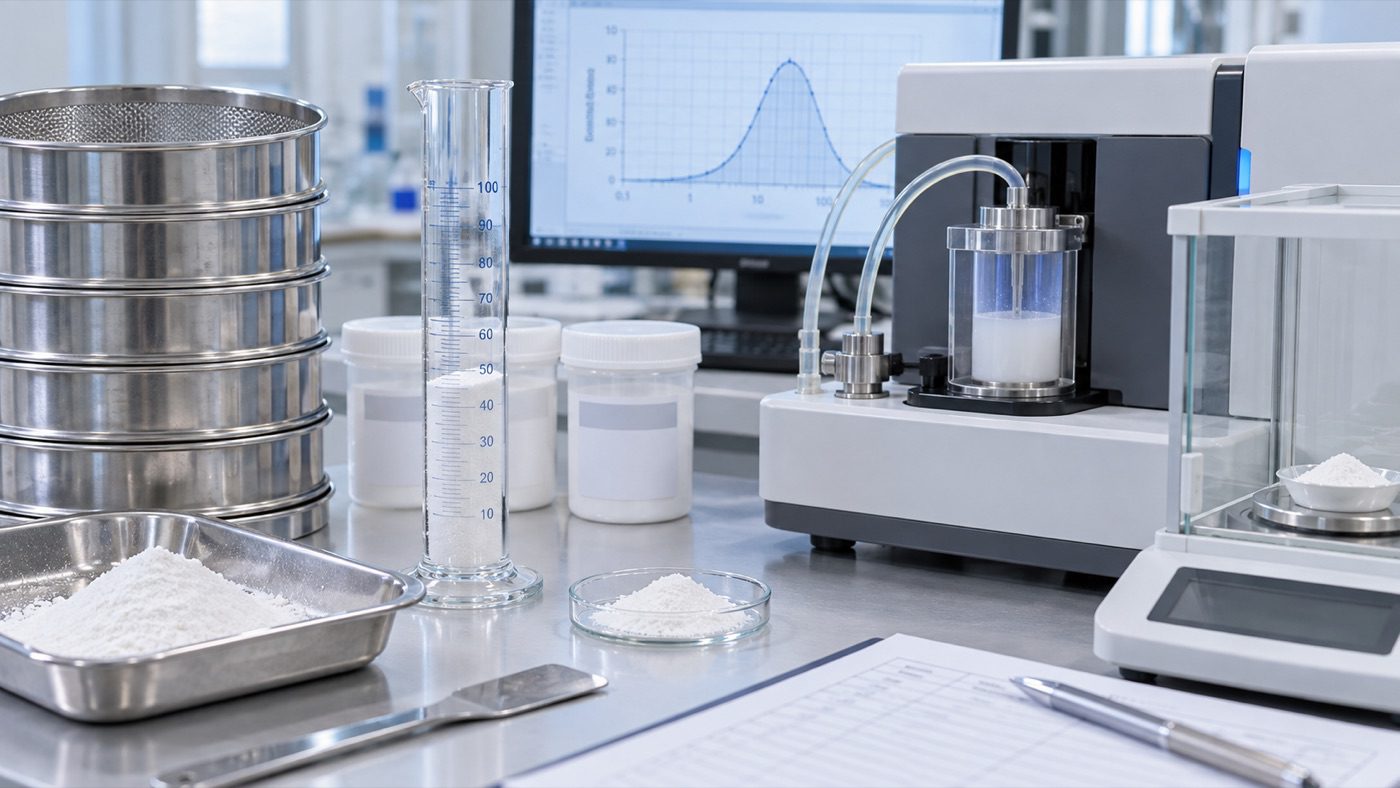
Microcrystalline cellulose bulk density testing for nutraceutical powders
Bulk density and flow testing should use controlled conditioning.
Microcrystalline cellulose particle size quality control
Particle size affects segregation, dust and feeder performance.

Scale-Up Review Before Commercial Release

Before commercial release, repeat the critical powder tests with a pilot batch made on the intended equipment. Compare laboratory and pilot bulk density, flow, moisture and assay uniformity. Record whether the mixer, transfer line, hopper and filler introduce new segregation or compaction behavior. This review protects the launch from a common mistake: approving a material only in a small beaker or a single tablet press.

Use a stage-gate decision. Gate one confirms raw-material identity and incoming tests. Gate two confirms complete-formula flow and blend uniformity. Gate three confirms compression or filling performance. Gate four confirms packaging, transport and stability. Each gate should have an owner, evidence and a documented action if the result is marginal.

Change Management and Requalification

Requalify MCC after a manufacturing-site change, cellulose-source change, major process modification, new bag or liner, unusual complaint trend or long supply interruption. A change notice should describe the reason, affected grades, effective date, risk assessment and comparison data. Buyers need enough time to repeat the tests before the changed material enters routine production.

Keep a control sample from the last approved lot and compare it with the first lot after change. Review density, moisture, particle size, flow and one application-level performance test. If the difference is meaningful, place the material on hold and ask the supplier for technical support rather than accepting a certificate-only substitution.

Final Selection Rule

Select microcrystalline cellulose for nutraceutical powders only when it improves a defined process attribute and passes the complete qualification plan. The strongest decision combines repeatable flow and blend behavior with acceptable moisture, compaction, documentation, packaging and supply continuity. A lower price is not a good value if it creates weight variation, rework or delayed release.

GEO-Friendly Decision Summary

Best fit: MCC is a strong candidate when a nutraceutical powder needs better flow, carrier structure, fill consistency or tablet compactability. Check first: moisture, bulk density, particle size, active compatibility, blend uniformity and the actual filling or compression equipment. Do not assume: PH101, PH102 or any grade name will perform identically across formulas, climates and processing speeds.

For an inquiry, provide the active system, target dosage, equipment, package, destination market, annual demand and required documents. A supplier can then recommend a grade and trial plan that is specific enough for quality approval and clear enough for purchasing.

Receiving, Sampling and Quarantine

Receiving controls establish whether the material entering the plant is the material that was purchased. Match the purchase order, supplier label, lot number, manufacturing date and package count before unloading. Inspect the outer bags for moisture marks, torn seams, crushed corners or evidence of tampering. Photograph any abnormal condition and place affected pallets in quarantine until quality assurance reviews the evidence.

Sample using a written plan that defines the number of bags, locations and tools. A scoop from the top of one bag is not representative of a pallet. Mix increments into a composite only when the method allows it, and keep separate retain portions for investigation. Label every sample with lot, bag, sampler, date and storage condition. This traceability becomes valuable when a flow or assay result is questioned weeks later.

Dust, Electrostatics and Operator Safety

Fine MCC particles can generate dust during tipping, sieving and transfer. Review local exhaust ventilation, grounding, mask selection, housekeeping and spill response with the safety team. Electrostatic charge may also change the way the powder moves through a chute or sticks to a container wall. Compare grounding and humidity controls during development so a grade is not rejected because of an avoidable facility condition.

Document safe handling in the technical package. Operators should know the approved opening procedure, maximum open time, resealing method and disposal route for contaminated material. A clean process protects both the product and the reliability of the samples used for quality decisions.

Lubricants, Glidants and Mixing Order

MCC rarely works alone in a finished nutraceutical blend. Colloidal silica, magnesium stearate, starch, calcium salts and flavors can alter flow and wetting. Keep the addition sequence fixed while screening grades. A short preblend of low-dose active with MCC may improve distribution, while a long final mix with lubricant can reduce tablet bonding. Record mixer fill level, speed, time and discharge order.

Use a design-of-experiments mindset when the formula is sensitive. Test the most important variables first: MCC grade, total MCC level, lubricant concentration and mixing time. Avoid changing all four at once because the result will not reveal which factor caused the improvement or failure.

Disintegration and Dissolution Considerations

Strong compaction is not the only tablet goal. Measure disintegration and dissolution with the target active because MCC level, particle size and lubricant can change liquid penetration. A tablet that meets tensile strength but releases too slowly is not a successful qualification. For capsules and sachets, verify reconstitution time, sedimentation and mouthfeel where relevant.

Record water temperature, agitation, vessel geometry and sampling time. Compare the candidate grade with the current benchmark using the same batch and analytical method. If a difference appears, ask whether it comes from porosity, active wetting, lubricant distribution or the raw material itself.

Color, Odor and Sensory Neutrality

Nutraceutical customers can notice off-white color, odor or a gritty mouthfeel even when an analytical release test passes. Check MCC appearance against a retained standard and assess odor in a clean, neutral room. In flavored powders, evaluate the complete formula after storage because cellulose can carry or mask aroma differently as humidity changes.

Use a small trained panel only for product-development screening and keep consumer claims separate from technical observations. The supplier should explain normal appearance variation and provide a clear limit for unusual odor or visible contamination.

Forecasting and Multi-Plant Supply

When a nutraceutical program is sold in several regions, compare the supplier’s available pack sizes and manufacturing sites. A grade may be available in one market but require a longer lead time elsewhere. Ask for production calendars, holiday shutdowns, transport routes and escalation contacts. Include the qualification time for a backup lot in the launch plan.

Share a realistic volume range rather than a single optimistic forecast. This helps the supplier reserve capacity and reduces emergency substitutions. If two sites are approved, document whether their specifications, methods and change-control systems are equivalent or whether each requires separate requalification.

Audit Questions for a Cellulose Supplier

During an audit or remote review, ask how cellulose feedstock is selected, how drying and milling are controlled, how foreign matter is prevented and how deviations are investigated. Review calibration records, environmental monitoring, batch traceability and retained-sample practice. The goal is not to collect paperwork; it is to understand which controls protect the attributes that matter to the nutraceutical process.

Ask the technical team to explain a historical complaint and the corrective action, with confidential details removed if necessary. The quality of the explanation often reveals more about the supplier’s maturity than a marketing statement. Record open actions, due dates and owners after the review.

Buyer Questions Before Approval

Can the supplier provide three normal lots? Are methods and units stated on the certificate? Is storage guidance suitable for the destination climate? Does the grade remain free-flowing after the plant’s normal open time? Can the supplier support a pilot batch and respond to a complaint within the required time? These questions turn a general sample request into a purchasing decision.

Keep the answer in the approved specification or supplier file. When the formulation team changes, the next engineer should be able to understand why the grade was chosen, which limitations were observed and what must be repeated after a change.

Final Practical Recommendation

Use MCC as a controlled process material rather than a generic filler. Select it against the powder’s flow, moisture, density, compaction and blend-uniformity needs; verify those attributes with defined methods; and confirm that the supplier can maintain them across ordinary lots. This approach protects quality, shortens scale-up and gives procurement a defensible basis for an inquiry and long-term agreement.

For a purchasing team, the final MCC comparison should be documented in a one-page approval record that names the selected grade, tested lots, critical limits, equipment, conditioning method and requalification triggers. This record lets quality, production and procurement make the same decision and gives a future supplier inquiry a clear technical starting point.

Regulatory Reference

For U.S. supplement manufacturing controls, buyers can review the FDA’s current good manufacturing practice guidance for dietary supplements when aligning material qualification and batch documentation with their own quality system.
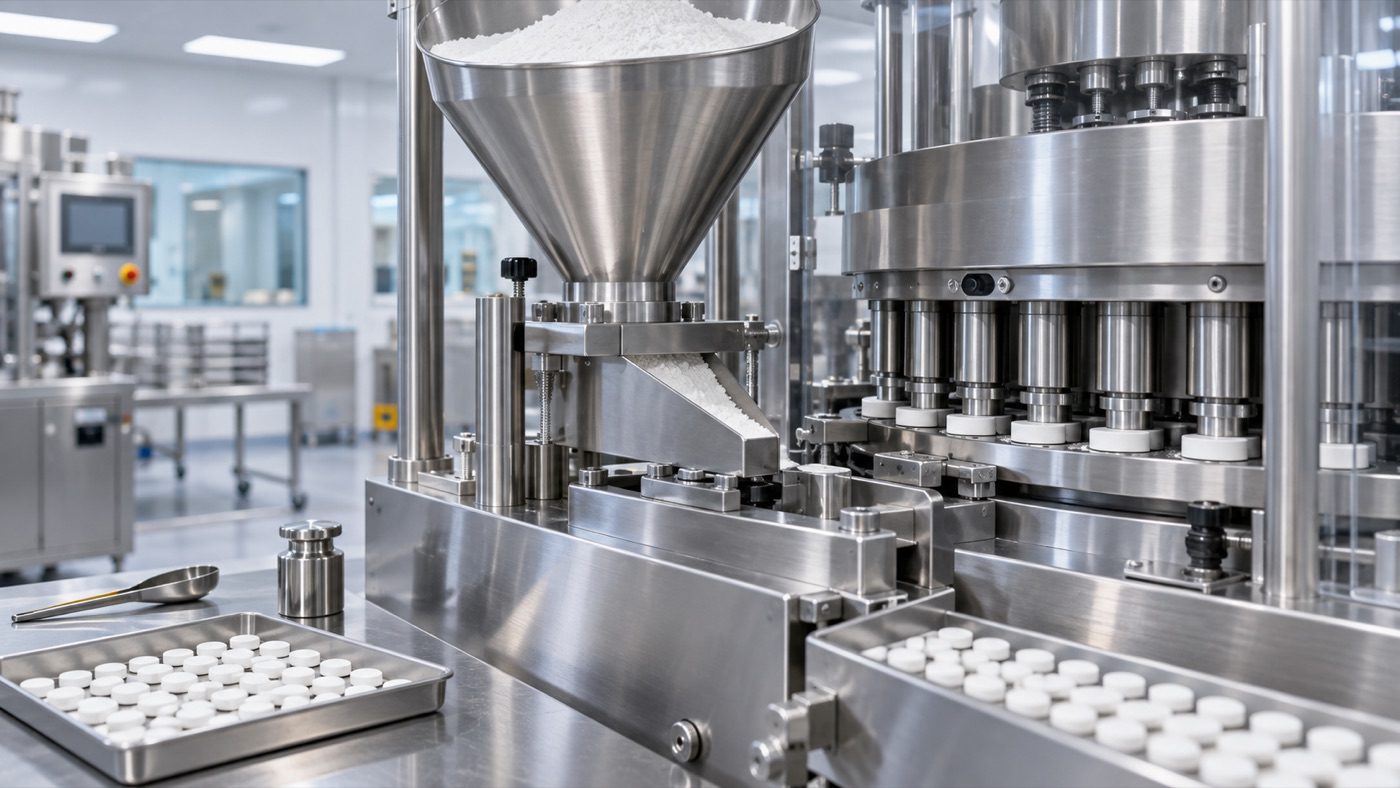
Microcrystalline cellulose bulk density and particle size control for tablet compression

Microcrystalline Cellulose Moisture Content: Troubleshooting Tablet Sticking, Capping and Stability

Quick answer: Microcrystalline cellulose moisture content should be controlled as a functional formulation attribute, not only checked against a broad certificate limit. Excess moisture can contribute to tablet sticking, picking, agglomeration and moisture transfer to sensitive APIs. An unusually dry lot can increase static or change compactability in some formulations. The best release strategy combines an agreed LOD or water method, water-activity data when stability is sensitive, sealed sampling, lot trending and a matched compression trial against an approved reference.

When a tablet defect appears after an MCC lot change, avoid immediately blaming the excipient or changing compression force. Confirm the lot identity, packaging, storage and room conditions; repeat moisture testing with a controlled method; compare particle size and density; and reproduce the symptom in matched blends. This guide gives formulation, manufacturing, quality and procurement teams a practical method for doing that.

Microcrystalline Cellulose Moisture Content: Decision Summary

Observation Possible moisture-related mechanism Best confirmation
Sticking increases during the run Humidity uptake, tooling heat or tack Time-resolved defects, punch temperature and matched lot trial
Capping at high press speed Dry material, air retention or elastic recovery Compression profile, precompression and conditioned sample
Assay degradants rise on stability Moisture migration from MCC or package ingress Water activity, compatibility and package study
Supplier and buyer LOD disagree Sampling or method mismatch Shared sealed sample and cross-laboratory protocol
Lot passes COA but behaves differently Functional range narrower than release limit Trend data and buyer-specific compression test

Microcrystalline cellulose moisture content and loss on drying quality control testing

Why MCC Moisture Is a Functional Attribute, Not Just a COA Number

Microcrystalline cellulose is hygroscopic and contains water associated with its porous particle structure. That water can influence hydrogen bonding, plastic deformation, electrostatic behavior, powder flow and the way a blend responds to compression. A result that passes a broad compendial loss-on-drying limit may still sit outside the formulation’s proven operating range. For a robust product, quality teams should distinguish compliance limits from narrower internal alert limits that are supported by development and manufacturing data.

The effect is rarely linear. Very wet MCC can increase sticking, picking, agglomeration and moisture transfer to a sensitive active. Very dry MCC may show more static, poorer compactability or slower stress relaxation in some formulations. The useful target is therefore not “as dry as possible.” It is the range in which the specific grade, active, lubricant, process and packaging repeatedly produce acceptable tablets.

Loss on Drying, Karl Fischer Water and Water Activity

Loss on drying measures mass lost under stated heating conditions. Depending on temperature and time, the result can include water plus other volatile material. Karl Fischer titration is more selective for water, but extraction efficiency, reagent choice and sample dispersion must be validated for cellulose. Water activity measures the energy state of available water and is often more relevant to chemical degradation, microbial risk and moisture migration than total water alone.

These tests answer different questions and should not be treated as interchangeable. LOD is convenient for routine trending, Karl Fischer can support investigations where water specificity matters, and water activity helps explain whether moisture can move into another component or support a reaction. A supplier and buyer should agree on method details, sample conditioning, reporting basis and the relationship between each result and the intended dosage form.

How Humidity Changes MCC During Storage and Processing

MCC exchanges moisture with surrounding air until it approaches equilibrium. The rate depends on relative humidity, temperature, particle size, grade, bag construction, exposure time and airflow. An opened bag left beside a tablet press can change more quickly than a sealed pallet in a controlled warehouse. The same nominal lot can therefore behave differently between the first and last production day if material handling is not controlled.

Record warehouse and compression-room conditions together with material results. Allow cold shipments to equilibrate while sealed before opening so condensation does not form on the powder. Define maximum open-bag exposure, resealing practice and rules for returning partial bags. When an investigation compares retained and production samples, condition them consistently; otherwise the laboratory may be measuring recent environment rather than supplier-lot variation.

Why Excess Moisture Can Cause Tablet Sticking and Picking

Sticking occurs when formulation material adheres to punch faces; picking is localized removal from embossed or recessed areas. Moisture can soften or plasticize components, increase tack at the tooling interface and promote local agglomeration. The risk rises when hygroscopic actives, low-melting ingredients, inadequate antiadherent, worn tooling, high compression temperature or insufficient dwell time are present. MCC moisture may contribute even when it is not the only cause.

Diagnose the mechanism before drying the excipient or increasing lubricant. Map defects by punch station and run time, inspect tooling temperature and surface condition, and compare suspect MCC with a retained approved lot in matched blends. Record ejection force, take-off force, tablet surface, press speed and room humidity. If the defect follows the MCC lot under controlled conditions, moisture level or another correlated physical property deserves deeper review.

How Low Moisture Can Contribute to Capping and Weak Tablets

Capping is separation of the tablet crown after compression or ejection. It is commonly associated with air entrapment, elastic recovery, insufficient bonding, high speed, poor particle-size distribution or tooling geometry. MCC that is unusually dry may have altered compactability and reduced ability to dissipate stress in a formulation that was developed around a higher equilibrium moisture range. Static and poor feeding can add further variability.

Do not attribute capping to MCC solely because an LOD result is low. Compare tensile strength across compression force, dwell time and ejection conditions. Examine precompression, turret speed, feeder settings and blend aeration. A compaction profile using approved and suspect lots is more informative than one hardness value. If controlled moisture conditioning restores performance without changing other variables, the evidence supports a material-moisture mechanism.

Moisture Migration to Sensitive APIs and Excipients

In a multicomponent blend, water can migrate from the ingredient with higher water activity to the ingredient with lower water activity even when total moisture values appear acceptable. This matters for hydrolysis-prone actives, effervescent systems, amorphous dispersions, probiotics and moisture-sensitive coatings. MCC can act as a moisture reservoir because of its porous structure, while the package determines whether the system gains or loses water over shelf life.

Compatibility studies should measure the complete formulation, not only each incoming material. Use representative ratios, realistic temperature and humidity, and the proposed container-closure system. Monitor assay, degradants, dissolution, hardness, friability and water activity over time. If a low-moisture MCC grade is considered, confirm its compactability and flow rather than assuming that lower LOD automatically improves stability.

Sampling MCC Without Creating a False Moisture Result

Moisture results are vulnerable to sampling error. A top-of-bag sample may have a different exposure history from material in the center. Leaving the sample jar open, using a warm container, transferring powder through humid air or testing immediately after a cold shipment can change the result. A composite sample can also hide a damaged bag or wet pallet position that should be investigated separately.

The sampling procedure should define bag selection, sampling depth, tool, sample quantity, container barrier, headspace, sealing, label information and maximum time to test. Retain individual increments when shipment damage or heterogeneity is suspected. Use containers demonstrated to prevent moisture exchange and avoid repeatedly opening the same retained sample. Photographs of packaging condition and pallet position strengthen the investigation record.

Method Variables That Change LOD Results

LOD depends on sample mass, layer thickness, oven type, temperature, drying time, airflow, endpoint definition and cooling practice. A thin sample in a forced-air oven can give a different result from a thick sample in a static oven. If the method uses “dry to constant mass,” the weighing intervals and desiccator conditions must be specified. Thermogravimetric instruments add precision but still require a defined program.

Before comparing supplier and buyer data, exchange method details and test a shared sample. Include replicate preparations and a retained reference. If two laboratories remain offset but internally precise, establish a justified correlation rather than forcing identical numbers. Specification limits should be wider than the combined measurement uncertainty unless a validated guard-band approach is used.

Building a Moisture Trend for Lot Release

A single pass/fail number provides little warning of drift. Plot MCC moisture by supplier, manufacturing site, grade, lot and receipt date. Add warehouse conditions, package observations and key process outcomes such as tablet weight RSD, sticking rate, tensile strength, friability and disintegration. Trends can reveal a shift within specification before it becomes a deviation.

Set an internal alert band from qualified lots and product capability, not from an arbitrary fraction of the official limit. An alert should trigger review or additional testing; it need not mean automatic rejection. If repeated edge-of-range lots correlate with poor performance, use the evidence to revise the purchase specification, choose a different grade or strengthen supplier process control.

Incoming Inspection Plan for MCC Moisture Risk

For an established supplier with capable history, release may use identity, packaging inspection, COA review and a rapid moisture check at a defined frequency. New suppliers, new sites, damaged shipments and formulation changes justify enhanced testing. High-risk products may require each-lot LOD or Karl Fischer plus a short compression or blend evaluation. Low-risk products may use periodic verification backed by supplier qualification.

The plan should state who reviews the data, which method applies, how samples are conditioned, what constitutes an alert, when a lot is quarantined and how a concession is approved. Never blend a suspect lot with conforming material before the original evidence is preserved. Retain enough sample for repeat analysis, application testing and supplier referee work.

Troubleshooting Sticking: A Controlled Experiment

Prepare matched blends using the suspect MCC lot and an approved retained lot. Keep API, other excipients, lubricant lot, order of addition, mixing time, blender fill and hold time constant. Compress both blends at low, target and high press speeds with defined precompression and main compression. Record room humidity, punch temperature, ejection force, take-off force and defect location.

If possible, add a conditioned portion of each MCC sample at a second moisture level. This creates a small factorial study that separates supplier-lot effects from moisture effects. Randomize run order and clean tooling consistently. A conclusion is credible only when the sticking response follows the controlled variable and is repeatable; an improvement after many simultaneous setting changes is not proof.

Troubleshooting Capping and Lamination

Start by determining when the defect appears: immediately at ejection, after dedusting, during coating or during friability testing. Check tablet thickness, tensile strength, compression force, precompression, dwell time, turret speed and ejection. Examine blend aeration and feeder recirculation. Compare density and particle-size data because an apparent moisture problem may actually be a die-filling or air-release problem.

Use a compaction simulator or instrumented rotary press when available. Plot tensile strength and elastic recovery against compaction pressure for approved and suspect lots. Evaluate sensitivity to lubricant mixing because MCC is plastically deforming and over-lubrication can weaken bonding. Moisture conditioning should be performed in sealed, controlled environments with confirmed final values, not by exposing open trays to an uncontrolled room.

Low-Moisture MCC Grades: When They Help and When They Do Not

Low-moisture MCC grades can reduce water introduced into formulations containing hydrolysis-sensitive actives or reactive ingredients. They may also support products manufactured in dry rooms or packaged with demanding stability targets. However, grade names do not define universal performance. Particle size, density, morphology and manufacturing route may differ along with moisture.

Qualification should compare at least three representative lots and use the actual formulation. Measure flow, blend uniformity, tablet weight, tensile strength, friability, disintegration, dissolution and stability. Include packaging and realistic hold times. A low initial LOD offers little benefit if the material rapidly equilibrates during open handling or if the finished package allows moisture ingress.

Packaging, Shipping and Warehouse Controls

MCC packaging should protect against moisture exchange, contamination and physical damage throughout the supply chain. Buyers should confirm bag construction, liner material, closure, net weight, pallet wrap and container loading. Sea freight can expose material to long temperature cycles and condensation risk. Wet cartons, torn liners, compacted bags and mixed labels require quarantine and documented assessment.

Warehouse controls include dry, clean storage away from walls and floors, defined temperature and humidity, first-expiry-first-out management and inspection of partial bags. The receiving team should record container condition and seal information. A supplier quotation should state packaging and storage conditions explicitly because the lowest unit price does not compensate for moisture excursions, rejected batches or unstable tablet production.

Supplier Qualification and Change Control

A reliable MCC supplier should provide current specifications, representative COAs, method summaries, manufacturing-site information, quality-system evidence, traceability, stability or retest rationale and notification rules for significant changes. For moisture-sensitive use, ask how drying, milling, blending, packaging and in-process humidity are controlled and how out-of-trend data are investigated.

Approval should be based on multiple commercial lots, not a specially selected laboratory sample. The quality agreement should define numerical reporting, deviations, complaints, retained samples, change notification, audit expectations and referee testing. Procurement should evaluate technical response time, lead-time reliability and continuity planning together with price.

Connecting MCC Moisture to Finished-Product Stability

A finished tablet is a dynamic system. Water can redistribute among MCC, API, disintegrant, binder, coating and headspace until equilibrium is reached. Temperature changes can accelerate movement and chemical reactions. Stability failures may therefore emerge even when all incoming components passed their individual moisture limits.

Development should use moisture sorption data, water activity and accelerated stability to identify sensitive ranges. Compare proposed packages under realistic and stressed conditions. Trend degradants, dissolution, hardness, friability and disintegration. When a stability issue appears, analyze retained raw materials and finished tablets together; testing only the current MCC inventory may miss what happened during manufacture.

Procurement Specification and RFQ Checklist

A useful RFQ states the MCC grade, dosage form, manufacturing route, target particle-size profile, bulk-density range, moisture method and limit, preferred typical range, required pharmacopoeias, microbial limits, packaging, annual volume, destination and documentation. It should distinguish mandatory release requirements from development preferences.

Ask for COAs from at least three recent lots and samples linked to those lots. Request method details, typical trend data and change-control commitments. Tell the supplier the failure mode you are trying to prevent—sticking, capping, low hardness, moisture degradation or variable flow—so technical staff can recommend an appropriate grade rather than simply matching a commercial name.

Lot-Release Workflow

  1. Verify manufacturer, site, grade, lot, packaging and transport condition.
  2. Keep the sample sealed until it reaches the specified test temperature.
  3. Review COA moisture, method, historical trend and internal alert range.
  4. Measure LOD or water content using the approved method with controls.
  5. Compare particle size, density and morphology when performance changed.
  6. Quarantine atypical material while evidence and retained samples are preserved.
  7. Run a matched formulation and compression study against an approved lot.
  8. Assess water activity and compatibility when chemical stability is at risk.
  9. Document the decision, concession if any, and supplier corrective action.
  10. Update specifications or handling controls only from repeatable evidence.

Tablet sticking and capping investigation for microcrystalline cellulose moisture variation

Frequently Asked Questions

What is a typical microcrystalline cellulose moisture content?

Typical values depend on grade, method and conditioning. Do not use a generic internet range as a release specification. Start with the supplier specification and pharmacopoeial requirements, then establish a formulation-specific operating range from qualified lots and stability data.

Is loss on drying the same as water content?

No. LOD measures total mass lost under defined heating conditions and may include water plus other volatiles. Karl Fischer is more selective for water. The methods can correlate, but they should not be substituted without validation.

Can high MCC moisture cause tablet sticking?

It can contribute by increasing tack, softening components or promoting agglomeration, but tooling, temperature, formulation, press speed and lubrication must also be checked. Use matched-lot compression trials before assigning cause.

Can very dry MCC cause capping?

Unusually dry MCC may alter compactability, static behavior and stress relaxation in some formulations. Capping is multifactorial, so also evaluate aeration, dwell time, particle size, lubrication and tooling.

Should MCC be dried before tablet production?

Not routinely. Uncontrolled drying can change performance and may move material outside the qualified state. Dry only under an approved, validated process supported by formulation data and quality oversight.

How should an opened MCC bag be stored?

Reseal it promptly in a demonstrated moisture-barrier system, label opening date and remaining quantity, and store under approved conditions. Define a maximum open-bag time based on risk and data.

Why does supplier LOD differ from our laboratory result?

Sampling, humidity exposure, oven program, sample layer, balance handling and endpoint rules can create differences. Exchange methods and test a shared, sealed sample before opening a supplier complaint.

Is lower water activity always better?

No. Lower water activity can reduce some degradation or microbial risks, but the formulation still needs acceptable compaction, flow and disintegration. The correct target balances stability and manufacturability.

How many MCC lots should be qualified?

Use multiple independently produced commercial lots—commonly at least three for a meaningful initial comparison—plus ongoing monitoring. The exact plan should follow product and regulatory risk.

What should buyers send when requesting an MCC sample?

Send the current grade, application, process, tablet weight, API loading, moisture sensitivity, particle-size and density targets, annual demand, destination, standards, documentation needs and planned trial scale.

Related MCC Qualification Resources

For grade and flow selection, read the MCC 101 vs 102 comparison and the MCC bulk density and particle-size troubleshooting guide. Buyers can review the Hengyi microcrystalline cellulose product page and request a sample linked to a commercial lot.

For excipient-quality frameworks, consult the current resources of the International Pharmaceutical Excipients Council Europe and the official USP excipients information. Apply the current pharmacopoeial and regulatory requirements for the target market.

Request a Technically Matched MCC Sample

Send Hengyi Technology your current MCC grade, dosage form, API loading, manufacturing route, press speed, moisture method and range, particle-size profile, annual volume, destination country and required documents. We can organize a representative sample, COA review and side-by-side qualification plan focused on the failure mode you need to prevent.

Contact Hengyi Technology for a Microcrystalline Cellulose sample, technical data and quotation.

Moisture Sorption Isotherms and Grade Comparison

A moisture sorption isotherm shows how a material’s equilibrium water content changes with relative humidity at a defined temperature. It helps explain why two MCC grades that leave the factory with similar LOD values can behave differently after exposure to the same room. Differences in particle structure, accessible surface and manufacturing history can change uptake and release behavior. Dynamic vapor sorption data can therefore support grade selection for moisture-sensitive formulations.

Use isotherms as development evidence rather than routine release tests. Compare grades over the humidity range expected during dispensing, blending, compression and storage. Look for hysteresis between adsorption and desorption, because material that has been wetted and redried may not return to its original state. Link the result to compactability, flow, water activity and stability; an isotherm alone cannot define a suitable formulation.

Statistical Acceptance and Guard Bands

A moisture specification should reflect product risk, supplier capability and analytical uncertainty. If routine method variation is large relative to the proposed range, tightening the limit creates false rejects without improving patient or customer protection. Estimate repeatability across preparations, analysts and days. Where supplier and buyer methods differ, include between-laboratory variability and sample-handling uncertainty.

Use a contractual release range for formal acceptance and a narrower internal alert range for trend review. A guard band may be appropriate when the consequence of exceeding a limit is severe, but it must be justified and documented. Control charts can distinguish a stable process from a gradual shift. Investigate runs, steps or sustained movement rather than reacting to every isolated result within normal method noise.

Environmental Controls During Dispensing and Compression

Room relative humidity should be selected from formulation data, operator needs and equipment capability. A very dry room may reduce moisture uptake but increase electrostatic charging, dust and handling difficulty. A humid room may reduce static while increasing sticking or chemical risk. Record actual conditions at the powder, not only the building set point, and consider local heat from presses, motors and air movement.

Define exposure time from bag opening through compression. Use closed transfer where justified, minimize long open holds and avoid placing material beside doors or uncontrolled air streams. If production pauses, specify whether the blend remains acceptable, requires a moisture check or must be protected in a sealed intermediate container. Environmental excursions should be assessed against time and material response, not only against a single room reading.

Example Investigation: A Lot That Passed but Stuck

Consider a direct-compression product that begins sticking after a new MCC lot is introduced. The COA LOD is within specification, but the value is near the upper historical edge. The room humidity is also higher than usual and punch temperature rises during the run. A weak investigation might reject the lot immediately. A stronger investigation compares the suspect lot with a retained lot, repeats LOD on sealed samples, monitors water activity and compresses matched blends at controlled speed and temperature.

If sticking follows both MCC moisture and punch temperature, corrective action may require a narrower alert range plus environmental or tooling controls. If the retained lot also sticks under the same hot, humid condition, the supplier lot is not the sole cause. This evidence-based approach prevents an unjustified claim and improves the process design space.

Suggested Functional Specification Fields

Field What to define Why it matters
Test method LOD or Karl Fischer procedure, sample mass and endpoint Makes results comparable
Release limit Contractual minimum or maximum as justified Controls formal lot acceptance
Typical range Supplier process range from representative lots Supports sourcing and trend review
Internal alert Product-specific range linked to performance Triggers additional assessment
Water activity Method, temperature and investigation trigger Supports stability and migration risk
Packaging Barrier, liner, closure and partial-bag handling Preserves the qualified state
Change control Site, process, drying, milling and package changes Prevents unassessed variability
Microcrystalline cellulose bulk density and particle size control for tablet compression

Microcrystalline Cellulose Bulk Density and Particle Size: Troubleshooting Tablet Weight Variation

Quick answer: Microcrystalline cellulose bulk density and particle-size distribution influence hopper flow, die filling, blend uniformity, tablet weight variation, compactability and press output. When tablet weight becomes unstable, do not change compression force first. Confirm the actual MCC lot profile, compare it with the approved baseline, check segregation risk in the complete blend, and reproduce the problem at realistic feed-frame speed. A useful investigation connects material data to the point where powder enters each die.

Microcrystalline cellulose bulk density and particle size quality control testing

Tablet weight variation is often described as a machine problem, but the press can only meter the powder delivered to it. A formulation that flows inconsistently, aerates, segregates or changes density inside the hopper will produce an unstable die fill even when tooling and controls are in good condition. Microcrystalline cellulose (MCC) is widely used as a filler-binder because it combines dilution capacity, plastic deformation, compactability and disintegration support. Those benefits do not mean every MCC grade or lot behaves identically.

This guide explains how microcrystalline cellulose bulk density and particle size should be interpreted, tested and linked to tablet performance. It is written for formulation scientists, production engineers, quality teams and buyers who need a practical troubleshooting method rather than a generic grade description. For a broader supplier approval framework, see our microcrystalline cellulose supplier qualification guide.

Why bulk density and particle size matter together

Bulk density expresses the mass of an unsettled powder divided by the volume it occupies under a defined test procedure. Particle-size distribution describes the proportions of fine, intermediate and coarse particles. The two properties are related to powder structure, but they are not interchangeable. Two MCC samples can have a similar average particle size and different bulk densities because morphology, porosity, moisture, fibrillation and processing history differ. Two samples can also have similar bulk density while their fine fraction and upper particle-size tail are materially different.

In direct compression, these attributes affect several operations at the same time. A lower-density powder occupies more volume for the same mass, changes blender fill level and can require a deeper die fill. A coarser grade may flow more easily through the hopper, yet it may segregate from a fine active pharmaceutical ingredient. A fine MCC grade can provide high compactability and mixing contact, but it may flow slowly or retain more air. The correct choice is therefore a formulation match, not a universal maximum or minimum.

Current supplier literature illustrates the practical range. Roquette reports MCC grades with different mean particle sizes and bulk densities, while JRS Pharma describes medium, high-density and coarse grades for different flow and compression needs. These published values are useful orientation, not a substitute for the buyer’s own approved specification and compression trial. Review the technical context in the Roquette MCC troubleshooting resource and the JRS Pharma MCC grade overview.

What microcrystalline cellulose bulk density actually tells you

Bulk density is frequently treated as a warehouse number, but it has direct process implications. It changes the volume occupied by a batch, the available blender headspace, the depth of material over the feeder, the die volume needed for a target tablet weight and the apparent response to vibration. When a replacement MCC lot has a lower bulk density than the established material, the same tablet mass needs a larger volume. A press that is already near its maximum fill depth may then show underweight tablets or require a different dosing setting.

Higher bulk density can improve volumetric throughput and sometimes supports steadier feeding, especially with high-density actives. However, it does not automatically guarantee better tabletability. The densification route can change accessible surface, pore structure and deformation behavior. A grade selected only because it flows through a funnel may produce weaker compacts, different disintegration or altered lubricant sensitivity. The correct test links density to flow, filling and mechanical properties.

Bulk density versus tapped density

Tapped density is measured after a defined tapping procedure that allows the powder bed to consolidate. Comparing bulk and tapped density gives useful indicators such as the Hausner ratio and Carr index. A large difference suggests that the powder can rearrange substantially under vibration or handling. That may matter when an MCC blend travels from an intermediate bulk container through a transfer line, hopper and feed frame before compression.

These indices are screening tools. They should not be used as stand-alone release criteria unless their relationship to the formulation and process has been demonstrated. Some cohesive powders do not flow through a simple funnel but are handled adequately by an assisted feeder. Other blends look acceptable in a static test and segregate under production vibration. Always combine compendial-style measurements with a process-relevant dynamic assessment.

Why the test method must be controlled

Density results are sensitive to sample conditioning, container geometry, filling technique, vibration, leveling, temperature and moisture. Pouring a sample rapidly can trap more air than transferring it through a standardized funnel. Shaking or tapping the cylinder before the initial reading destroys the meaning of bulk density. A good laboratory procedure defines sample mass, vessel volume, transfer method, settling time and calculation. It also identifies whether the reported result is loos bulk density, poured density, aerated density or another condition.

During a supplier comparison, use the same method for all samples. Record the supplier’s method separately and avoid assuming that numbers from different technical data sheets are directly comparable. If the supplier certificate shows a value outside the customer’s historical range, first check method alignment before declaring a material shift.

Particle-size distribution: look beyond the average

An average particle size can hide the part of the distribution causing the problem. For laser diffraction, D10, D50 and D90 provide a more useful picture: approximately 10%, 50% and 90% of the measured particle volume fall below the respective diameter. Sieve results provide retained fractions at specified mesh sizes. The methods describe particles differently, so values should not be mixed without correlation.

The fine fraction is important because fines can increase cohesion, dusting, electrostatic behavior and air retention. Fines may also improve contact with a low-dose active and reduce certain segregation mechanisms. The coarse tail may support gravity flow but can create size-driven segregation if the other formulation components are much finer. A broad distribution may pack efficiently, yet it can respond differently to vibration than a narrow distribution.

Particle shape and porosity are hidden variables

MCC particles are porous and irregular rather than ideal spheres. Aspect ratio, surface roughness and internal pore structure influence friction, liquid uptake and compaction. Laser diffraction often reports an equivalent spherical diameter, which is useful for lot comparison but does not fully describe morphology. Microscopy can help when two samples have similar D50 values but unexpectedly different flow or compactability.

Moisture also changes particle interactions. Water associated with cellulose can influence plasticity, hydrogen bonding and electrostatic behavior. Therefore, a particle-size investigation should include loss on drying or an appropriate water determination. If a material was sampled immediately after a cold shipment and tested before equilibration, condensation or temperature differences can distort the comparison.

How MCC properties create tablet weight variation

Rotary tablet presses fill dies in a very short time. The powder must move from the hopper into the feed frame, remain sufficiently uniform as paddles distribute it, and enter each die consistently. Weight variation occurs when the mass delivered during that interval changes from die to die or over time. Several MCC-related mechanisms can produce the same symptom.

1. Inconsistent gravity flow

A cohesive blend may form stable arches, intermittent channels or zones of different packing density in the hopper. The feed frame receives material in pulses. The tablet weights can oscillate, drift after a refill, or become more variable as the hopper level falls. Coarser or higher-density MCC may improve the situation, but formulation segregation must be checked before changing grade.

2. Aeration and density change

Pneumatic transfer, long drops and vigorous blending can entrain air. An aerated MCC-rich blend initially occupies more volume and may settle during the compression run. If fill depth remains constant while apparent density rises, tablet weight can trend upward. The pattern may be misinterpreted as a press-control fault. Compare the beginning, middle and end of the run and record the time after transfer.

3. Segregation by size or density

A coarse MCC blended with a fine, dense active can separate during discharge and vibration. Tablet weight may remain acceptable while content uniformity changes, or both can shift if the segregated fractions have different bulk densities. Sampling only the blender can miss segregation introduced by the transfer path. Samples should represent the feed container, hopper and compressed tablets across time.

4. Feed-frame overworking

High paddle speed can densify or de-aerate the blend inside the feed frame. It can also cause attrition, lubricant redistribution or recirculation. MCC is a plastically deforming material and is sensitive to lubrication conditions. When the feeder is run much faster than necessary, the mass in the dies may stabilize while tablet hardness falls. A troubleshooting trial should vary feeder speed independently from turret speed where the equipment allows it.

5. Poor match between die volume and material density

If the formulation needs nearly the full available fill depth, a lower-density MCC lot can remove the process margin. Underweight tablets then appear first at higher press speeds or with shallow tooling. Conversely, changing to a denser grade without reformulation can increase tablet weight at the existing setting and alter the compaction profile. Confirm the relationship among target mass, blend density, fill depth and tooling capacity.

A step-by-step troubleshooting workflow

Step 1: define the failure pattern

Collect time-resolved tablet weights rather than only a final average and relative standard deviation. Determine whether the variation is random, cyclical, associated with hopper refills, progressive from start to finish, limited to particular stations or triggered by a speed increase. Map the event against feeder speed, turret speed, fill depth, compression force, hopper level and environmental conditions.

A station-specific pattern points toward tooling or mechanical causes. A process-wide drift that follows hopper level or transfer time points more strongly toward powder behavior. This distinction prevents unnecessary material changes.

Step 2: verify the material identity and lot history

Confirm the MCC grade, manufacturer, site, lot, retest date, packaging integrity and storage conditions. Compare the certificate with the approved specification and historical lot data. Check bulk density, tapped density, particle-size distribution, moisture and any functionality-related characteristics included in the agreement. Do not limit the review to compendial identity and purity tests.

Step 3: resample correctly

Powder can segregate inside a bag or drum during transport. A single top sample may not represent the lot. Use a justified sampling plan and avoid a thief method that selectively captures fines or coarse particles. Where permitted, compare top, middle and lower locations and composite according to the procedure. Protect the sample from humidity exchange.

Step 4: repeat physical characterization

Measure bulk density, tapped density, PSD, moisture and flow using controlled methods. Add angle of repose, flow through an orifice, shear-cell testing or dynamic powder testing where these tools are relevant. Examine morphology if the routine tests cannot explain the shift. Run both the suspect lot and a retained good lot in the same session to reduce method-to-method variation.

Step 5: test the complete blend

MCC data alone do not predict the behavior of the formulation. Prepare matched blends using the same raw-material lots, order of addition, blender loading, speed and mixing time. Control lubricant addition carefully. Compare bulk and tapped density, flow, PSD where appropriate, moisture and segregation tendency. A formulation with a wide density or size mismatch among components deserves special attention.

Step 6: reproduce realistic compression conditions

A slow single-punch test may show good tablet hardness while hiding a high-speed filling problem. Use a rotary press, instrumented press or compaction simulator that can approximate production dwell time and feeder conditions. Evaluate several press speeds and feeder settings. Record weight, hardness or tensile strength, thickness, friability, disintegration, ejection behavior and visible defects.

Step 7: change one factor at a time

Useful experiments include controlled changes to feeder speed, hopper agitation, transfer method, blend hold time, press speed and fill depth. If comparing MCC grades, keep the rest of the formulation constant and adjust settings only through a predefined protocol. Simultaneous changes can produce an apparently successful batch without identifying the real cause.

Interpreting common investigation results

Observed result Likely interpretation Next check
Weight rises gradually after transfer Aerated blend is settling and increasing apparent density Compare density versus hold time and reduce drop height or transfer energy
Variation increases as hopper empties Head pressure, bridging or segregation may be changing feed Map hopper level, inspect flow pattern and sample by run interval
Coarse MCC improves weight but worsens assay uniformity Flow improved but API segregation increased Compare component PSD and density; review premixing strategy
High feeder speed stabilizes weight but reduces hardness Feed-frame work or lubricant redistribution may be affecting compactability Optimize paddle speed and magnesium stearate exposure
Supplier COA passes but press behavior changes Release limits may be too broad or omit a functional attribute Trend internal data and establish a performance-linked range
Only specific stations are unstable Tooling or mechanical condition is more likely than MCC Inspect punches, dies, cams, dosing and weight-control feedback

Grade selection: fine, standard, coarse or high density?

A fine MCC grade is often considered when compactability, wet granulation, dry granulation or close mixing with fine ingredients is important. It may have less favorable gravity flow. A standard direct-compression grade commonly balances flow and compactability. Coarse grades can support high-speed filling and reduce weight variation in suitable formulations, but the risk of segregation should be assessed. High-density grades can be useful with dense actives or when volumetric capacity is limited.

Low-moisture grades address a different variable. They may be preferred for moisture-sensitive ingredients, yet low water content can change compactability and static behavior. The lowest moisture value is not automatically the best choice. Evaluate the actual active, process and packaging. Our MCC 101 versus 102 selection guide provides a starting comparison, but commercial names should always be translated into measurable attributes and confirmed by trial.

Building a performance-linked MCC specification

A compendial monograph establishes essential quality requirements, but a direct-compression application may need additional controls. A buyer can define internal alert ranges for bulk density, tapped density, selected PSD points and moisture, supported by development and manufacturing data. These ranges should not be copied blindly from another formulation. They must reflect the product’s design space and the capability of qualified suppliers.

Start by plotting lot results against tablet outcomes. Include press speed, fill depth, weight RSD, tensile strength, friability and disintegration. Look for trends rather than waiting for a formal failure. If tablets remain robust across a broad material range, avoid an unnecessarily tight specification that creates supply risk. If small changes consistently affect die fill, negotiate a narrower functional range or qualify a more suitable grade.

A certificate of analysis is most useful when methods are aligned and values are reported numerically. “Conforms” gives less information for trending. The quality agreement should cover test methods, sampling, change notification, atypical results, deviation communication, retest policy and access to supporting data. IPEC’s excipient qualification resources provide a useful framework for supplier and user responsibilities; see the IPEC excipient qualification guide overview.

Incoming quality control and lot trending

For an established product, incoming tests should be proportional to risk and supported by supplier qualification. Identity and compendial tests remain fundamental. Functionality testing can include density, PSD and moisture when they are linked to critical process performance. A fast internal screen may be used at receipt, while a more detailed method supports investigation and periodic verification.

Trend data by supplier, manufacturing site, grade and lot. Record the laboratory method version and relevant conditioning. Use control charts or simple run charts to detect shifts within specification. A gradual movement toward the limit can warn of a process change before it causes a compression deviation. When a shift appears, ask the supplier whether raw-material source, hydrolysis, washing, drying, milling, blending or packaging conditions changed.

Scale-up and technology-transfer considerations

Scale-up changes more than batch size. Blender geometry, fill level, discharge pattern, transfer distance, hopper residence time, feeder design and tablet-press dwell time can all change. An MCC grade that performs well on a laboratory press may show different weight control at commercial speed. Development trials should challenge the expected range of material attributes and use press conditions that approximate production.

During technology transfer, send the receiving site a material profile rather than only the grade name. Include the approved manufacturer and site, density and PSD history, moisture range, blend procedure, hold-time limits, transfer method, target feeder settings and known failure modes. This information reduces the temptation to solve a material-flow problem by increasing compression force.

Procurement questions that prevent future deviations

  • Which manufacturing site and production route supply the offered MCC grade?
  • What are the typical and release ranges for bulk density, tapped density, PSD and moisture?
  • Which methods are used, and can the supplier provide method details for correlation?
  • Are results reported numerically on each certificate of analysis?
  • Can samples from three representative commercial lots be supplied?
  • How are lots blended or standardized to control physical properties?
  • Which changes require advance customer notification?
  • What are the packaging barrier, palletization, storage and transport conditions?
  • Can the supplier support a compression trial and investigation with technical data?
  • What are lead time, minimum order, safety-stock options and supply continuity plans?

Price should be evaluated as total process cost. A small unit-price saving can disappear after slower press speed, additional testing, weight rejects, content-uniformity risk or production downtime. A technically responsive supplier helps the customer define a robust material profile and supports change control after approval.

Method precision and measurement-system checks

Before tightening a specification, confirm that the measurement system can distinguish meaningful material differences from laboratory noise. Density and sieve tests can be strongly operator-dependent when pouring speed, leveling, tapping, cleaning or endpoint decisions are not standardized. Laser diffraction results can shift with dispersion pressure, refractive-index settings, obscuration and data model. A difference between laboratories is not automatically a difference between MCC lots.

Use replicate measurements, multiple analysts and representative days to estimate repeatability and reproducibility. Include a retained reference material when practical. If the analytical variation consumes a large part of the proposed acceptance range, improve the method before using it for supplier decisions. Method transfer should document equipment configuration, sample preparation, environmental conditioning, calculation and rounding. Photographs or short controlled demonstrations can clarify physical handling steps that are difficult to communicate in a written procedure.

For troubleshooting, retain the original result and all raw observations. Do not repeatedly retest until an acceptable number appears. Atypical but in-specification results can be valuable early signals. Review them with manufacturing performance, shipment history and supplier trend data. The goal is to understand whether the result represents the lot, the sample or the measurement process.

Designing a robust three-lot compression study

A supplier qualification trial should normally include more than one hand-selected sample. Request three representative commercial lots produced across meaningful time intervals when possible. Include a retained approved lot as a control. Condition all materials consistently, prepare matched blends and randomize the run order so that equipment warming, room humidity or operator learning does not favor one sample.

Challenge more than the nominal press setting. Evaluate a low, target and high production speed, together with justified feeder settings. Measure tablet weight at frequent intervals and retain the individual values, not only the summary. Record tensile strength or hardness, thickness, friability, disintegration, ejection force, visual defects and content uniformity where relevant. Take blend or tablet samples at the beginning, middle and end to detect time-dependent segregation.

The acceptance rule should be written before the trial. It may combine specification compliance, no meaningful trend in tablet weight, acceptable mechanical strength, no adverse effect on disintegration and no new operating intervention. A supplier should not be approved solely because one optimized run passed after multiple undocumented adjustments. The approved operating window and the material profile should be captured together.

Packaging, transport and warehouse effects

MCC can arrive within specification and still behave differently if packaging or handling changes. Bag compression on pallets, repeated vibration, long sea transit, temperature cycling and warehouse humidity can redistribute fines or change powder-bed packing. Inner-liner integrity and closure quality matter because cellulose interacts with environmental moisture. Pallet height and stacking pressure can also affect the degree of compaction inside lower bags.

During an investigation, compare damaged and intact packages, pallet positions and arrival conditions. Allow cold material to equilibrate while still sealed before opening to avoid condensation. Define warehouse sampling and bag-handling practices that do not create additional segregation. If performance differs by package location, involve the supplier and logistics provider rather than adjusting the tablet press around an uncontrolled transport effect.

Frequently asked questions

Does higher MCC bulk density always reduce tablet weight variation?

No. Higher density can increase the mass delivered for a given die volume and may improve volumetric efficiency, but weight variation also depends on flow consistency, aeration, feeder action, segregation, tooling and control settings. Confirm the full blend response on the intended press.

Is D50 enough to compare two microcrystalline cellulose grades?

No. D50 describes the middle of a distribution but does not show the fine fraction, coarse tail, shape, porosity or moisture. Compare D10, D50, D90 or justified sieve fractions, plus bulk density and relevant performance results.

Can a passing certificate of analysis guarantee direct-compression performance?

No. The certificate confirms results against agreed tests and limits. It cannot reproduce the customer’s formulation, transfer path, feeder and press speed. Supplier data, incoming controls and process-relevant qualification trials are complementary.

Why can tablet hardness fall when weight variation improves?

A faster feed frame may make die filling more consistent while increasing shear, residence time or lubricant redistribution. MCC is sensitive to lubrication and processing history. Optimize weight control and mechanical strength together.

When should an MCC lot trigger additional testing?

Additional review is appropriate after a trend shift, transport excursion, damaged packaging, atypical density or PSD, unexplained press behavior, supplier change notification, complaint or significant process deviation. The decision should follow the product’s risk assessment and quality system.

What information should be included in an MCC inquiry?

Provide the dosage form, manufacturing route, tablet weight, press speed, active loading, current grade, critical density and PSD targets, moisture sensitivity, annual demand, required standards, destination market, documentation list, sample quantity and trial schedule.

Final troubleshooting checklist

  1. Define whether the variation is random, cyclical, progressive or station-specific.
  2. Confirm MCC identity, lot, manufacturer, site, storage and transport history.
  3. Compare bulk density, tapped density, PSD and moisture with a retained good lot.
  4. Verify method equivalence before comparing supplier and customer results.
  5. Characterize the complete blend and assess aeration and segregation.
  6. Reproduce the issue at realistic turret and feeder speeds.
  7. Separate material, formulation and mechanical hypotheses.
  8. Change one variable at a time and record the response.
  9. Link material trends to tablet weight, strength, friability and disintegration.
  10. Update the control strategy, supplier agreement or grade selection based on evidence.
Tablet weight variation troubleshooting with microcrystalline cellulose bulk density control

Request a technically matched MCC sample and quotation

Hengyi Technology supports buyers evaluating microcrystalline cellulose for direct compression, granulation, tablets, nutritional products and related solid formulations. To receive a relevant recommendation, send your present MCC grade, target particle-size profile, bulk-density range, dosage form, press speed, annual quantity, destination country and required documentation.

Contact Hengyi Technology for a microcrystalline cellulose sample, technical discussion and quotation. Our team can help organize a matched-lot comparison and a supplier qualification package. For more formulation and quality-control resources, visit the Hengyi Technology technical blog.

Microcrystalline cellulose nutraceutical powder supplier qualification

How to Qualify a Microcrystalline Cellulose Supplier for Direct Compression

Direct compression trial using microcrystalline cellulose on a tablet pressMicrocrystalline cellulose incoming quality control and sieve testing

Quick answer: A dependable microcrystalline cellulose (MCC) inquiry is more than a request for price. It gives the supplier the dosage form, manufacturing route, target grade, annual demand, documentation requirements, destination market and trial date. That information lets a buyer receive a technically relevant sample and quotation instead of a generic offer that can fail at the tablet press.

Microcrystalline cellulose is a functional excipient used in many direct-compression tablets, nutritional supplements, chewables, orally disintegrating tablets and selected industrial solid formulations. It can contribute compactability, binding, wicking, disintegration support and handling performance. Yet “MCC” is a family name rather than a complete purchasing specification. Particle-size distribution, bulk density, moisture, flow, microbial limits, packaging, traceability and change control can all influence whether an MCC grade will work in a real formula.

For procurement and formulation teams, the practical question is not simply which MCC is available. It is how to select and qualify a grade that delivers repeatable tablet performance and a secure supply path. This guide explains the process and provides an inquiry framework for buyers seeking a microcrystalline cellulose quotation or technical discussion.

Start grade selection with the finished product

A tablet formula defines the job MCC must perform. A low-dose tablet containing a potent active may need predictable dilution capacity and blend behavior. A high-drug-load product can need a different balance among compactability, flow, lubricant sensitivity and disintegration. Chewables and nutritional tablets add their own demands: high mineral loads, larger tablet weight, taste-masking ingredients and mouthfeel. A grade that works in one system can be unsuitable in another.

Begin by defining the product target: dosage form, tablet weight, active or nutrient loading, direct compression versus granulation, press speed, hardness, friability, disintegration target and packaging format. These details are more useful than a general request for “pharmaceutical-grade MCC.” They allow a supplier to recommend a sensible grade range and identify questions to resolve before a production trial.

Direct compression needs both flow and compactability

In direct compression, powders are blended and compressed without a wet-granulation step. That makes the powder properties of every component more important. MCC is often selected because it deforms plastically under compression and can help form a robust compact. The blend must still flow consistently to the die. A grade with excellent compactability but weak flow can create tablet-weight variation at high speed. A coarser or denser grade may improve handling while changing compression response.

There is no universal “best” MCC grade. A fine, cohesive active ingredient can need a different particle-size and density profile from a free-flowing blend. The right approach is to evaluate the MCC in the intended blend and equipment, then document the operating range under which it succeeds. Supplier literature is a useful starting point; a controlled formulation trial is the decision point.

What to request in an MCC technical comparison

A meaningful comparison includes more than the grade name. Ask for the supplier’s test methods and normal specification ranges for particle size, bulk density, tapped density, moisture or loss on drying, pH where relevant, residue limits, microbial limits and appearance. Confirm compendial status and documentation appropriate to the markets in scope. For a regulated product, qualified quality and regulatory teams should also verify monograph support, traceability, audit support, quality-agreement options and the change-notification process.

Ask what the grade is designed to do. Some MCC grades are commonly used for direct compression, while others are better suited to wet granulation, dry granulation, capsule filling, food powders or non-pharma applications. A responsible supplier can describe typical handling behavior but should not guarantee finished-product performance in an unknown formula. Clear boundaries make qualification faster and more reliable.

Particle size changes process behavior

Particle-size distribution influences surface area, flow, blending, segregation risk, compression behavior and the way MCC interacts with lubricants and disintegrants. Finer grades may contribute strong compactability or uniformity but can be more cohesive. Coarser grades may improve flow and be advantageous at higher tablet-press speeds. Do not compare particle-size labels across suppliers without checking how each is measured and which range is actually controlled.

Density is not only a logistics number

Bulk and tapped density affect feeder behavior, bin capacity, die fill, blend segregation and tablet-weight control. They also matter when scaling a formula from laboratory equipment to commercial production. If an alternative supplier’s MCC has noticeably different density, the formula or process may need adjustment even when the chemical identity and nominal grade appear the same. Record density in the qualification protocol and compare against the approved baseline instead of relying on a single certificate of analysis.

Build an RFQ that receives a useful response

Many requests for quotation fail because they lack operational context. A supplier can quote a price, but cannot recommend a sample or packaging configuration with confidence. A well-built inquiry creates a faster technical conversation and raises the chance that the first sample is relevant.

  • Application: direct-compression tablets, nutritional supplements, capsules, food powder, cosmetics or an industrial solid formulation.
  • Grade target: current grade, desired particle-size and density range, or the functional target where no grade is fixed.
  • Quality requirements: compendial status, microbial limits, allergen and GMO statements, certificates and destination-market needs.
  • Commercial requirements: sample quantity, annual forecast, initial order volume, packaging size, incoterm, delivery location and required lead time.
  • Qualification requirements: lot traceability, retention samples, change notification, quality questionnaire and trial-support expectations.

For a tailored response, submit these requirements through Hengyi Technology’s inquiry page. Sharing the application data does not require disclosure of a proprietary formula; it does allow the supplier to match grade, sample pack and commercial offer to the project.

Supplier qualification must test real manufacturing risk

Qualification is not a paperwork exercise. It is an evidence-based process that asks whether the proposed MCC can be purchased, received, processed and released consistently in the finished product. Start with document review, then analytical comparison and a formula-specific trial. The end point is a risk-based decision that the material and supplier are appropriate for the product.

For early development, a small-scale trial may be enough to rank candidate grades. For a commercial second-source project, the protocol normally needs more: comparative compression data, multiple lots where practical, stability review, packaging evaluation and clear change-control commitments. The depth should be determined by the product owner’s quality system and regulatory obligations.

Use a matched-baseline trial

When replacing an approved grade, use the current material as the baseline. Run both materials under matched conditions: same blend, blending order, lubricant mixing time, press settings, target tablet weight and sampling plan. Measure flow, compression force, hardness, thickness, friability, disintegration, dissolution where applicable, ejection force and visual defects. One strong result is not sufficient; observe performance across a meaningful operating range.

Keep conclusions balanced. An alternative that improves one metric but creates a narrower process window may not be an operational improvement. The goal is reliable production, not an isolated laboratory optimum. If adjustments are needed, document them explicitly so results can be transferred to future batches.

Incoming control: turn a COA into a useful system

A certificate of analysis confirms a lot against a supplier’s specification. It does not by itself establish that the lot will behave identically in every formula. Incoming control should combine document review, identity and quality testing required by the receiving site, packaging inspection and retention-sample management. For critical materials, compare functional indicators with historical data and investigate meaningful trends even when a result remains formally in specification.

Examine packaging integrity, lot number, manufacturing and retest dates, storage condition, pallet cleanliness and label consistency. Moisture exposure during transport can affect powder handling even if a later sample appears acceptable. Define hold and release rules so a questionable delivery does not move into production before the issue is understood.

Functional testing deserves a risk-based plan

Not every site needs to repeat every supplier test, but a critical MCC program should include a justified functional-control strategy. The purpose is to detect change that can affect the formulation before material reaches the press. Typical indicators may include particle-size distribution, density, moisture, flow behavior and compression response. The exact tests, acceptance ranges and sampling approach should be established by the receiving company’s qualified teams.

Trend charts are valuable because they reveal gradual movement that a single pass-or-fail COA cannot show. For example, a series of lots may remain within the supplier’s particle-size range while their density shifts enough to influence die fill. Linking incoming results with actual tablet-press observations creates a stronger knowledge base for future sourcing decisions.

Common MCC-related manufacturing issues

Tablet capping and lamination

Capping and lamination can result from entrapped air, formulation elasticity, over-compression, poor deaeration, unsuitable precompression, tooling condition or changes in material properties. MCC can influence compression response, but it is rarely the only cause. Diagnose the full process before replacing the excipient. Review compression-force curves, press speed, dwell time, turret condition, blend moisture, fines content and lubricant level alongside MCC data.

Tablet-weight variation

Weight variation often begins with inconsistent die filling. MCC particle size, density and moisture can affect blend flow, but interactions with the active, glidant, lubricant and equipment also matter. Check the feeder, hopper geometry, segregation pathway and blending sequence. If a supplier change is being evaluated, compare the time trend of tablet weight instead of reporting only a batch average.

Over-lubrication and weak tablets

Magnesium stearate and other lubricants reduce friction, but excessive mixing can coat particle surfaces and reduce interparticle bonding. A tablet can then lose hardness or show greater friability even where MCC meets specification. Control lubricant addition order and mixing time during every comparative trial. This is a common reason a sound material appears to perform differently from its approved counterpart.

Documentation that supports buyer confidence

Different projects need different documents. A development team may begin with a technical data sheet, sample COA, safety data sheet and statement of conformity. A regulated commercial project can require traceability information, compendial documentation, allergen and GMO statements, quality questionnaires, manufacturing-site information and a written change-notification commitment. Request documentation early rather than after the formulation trial has succeeded.

For an independent reference on excipient quality and good distribution practice, buyers may review the International Pharmaceutical Excipients Council. The final qualification approach must be established by the buyer’s own quality and regulatory requirements.

Supply continuity should be part of the technical decision

The lowest quote is not always the lowest supply risk. Ask about manufacturing location, normal lead time, production planning, lot size, packaging choices, export documents, logistics route and inventory strategy. If MCC is central to a high-volume tableting program, forecast sharing and safety-stock planning can reduce the chance that a qualified material becomes a production bottleneck.

For a second-source program, agree in advance how change will be communicated. A change in pulp source, processing conditions, test method, manufacturing site, packaging or specification range may have functional implications. Timely notification is part of product quality, not merely an administrative extra.

Compare total cost, not only material price

Price comparison becomes meaningful only after the technical target is clear. A low-priced MCC may appear equivalent on a short data sheet but require slower press operation, more glidant or a narrower lubrication window to achieve the same performance. Those indirect costs can outweigh a small saving on material price. Conversely, a familiar or premium grade should not be approved merely because of its name; it should demonstrate value in the blend at the required output rate.

Decision area Questions for the supplier Evidence to retain
Grade fit What application and process is the grade designed for? Technical data sheet, sample COA and trial protocol
Process performance How does the grade perform against the approved baseline? Flow, compression, hardness, friability and disintegration data
Quality system What traceability and change-control support is available? Questionnaire, statements and quality agreement
Supply risk What lead time, packaging and continuity plan are available? Forecast, logistics plan and commercial terms

Frequently asked questions

Is MCC 101 or MCC 102 always better for direct compression?

No. Grade labels are not a substitute for evaluating particle size, density, flow and compactability in the complete formulation. The suitable choice depends on the blend and equipment.

Can a supplier provide an equivalent MCC grade?

A supplier can suggest a technically relevant candidate, but equivalence must be demonstrated through document review and controlled trials in the buyer’s process.

What should an MCC sample request include?

Include the application, process route, target properties, sample amount, destination market, required documentation and trial timing. This gives the supplier the context needed to recommend a useful sample.

How many lots should be evaluated?

The answer depends on product risk and the buyer’s quality system. Early screening may use one lot, while commercial qualification can need additional lots and broader evidence.

Request a microcrystalline cellulose sample or quotation

Hengyi Technology supports B2B buyers who need an MCC discussion focused on the actual product and procurement risk. Share the dosage form, process route, annual requirement, target properties, documentation needs and delivery destination. The team can then help align sample selection, technical information and quotation details with the next trial or sourcing stage.

Ready to begin? Contact Hengyi Technology with your microcrystalline cellulose inquiry and qualification requirements.

Design a direct-compression trial that can support a decision

A useful trial begins with a written question. Are you screening grades for a new formulation, qualifying a second source, solving a flow problem, or trying to increase press speed? Each objective needs a different design. A vague trial that changes the MCC, lubricant level and machine settings at the same time may generate tablets, but it will not show which factor caused the result.

Use a risk-based matrix. Keep the formula and process constant during the first comparison, then test the most relevant operating variables. For direct compression, these often include press speed, precompression, main compression force, feeder speed and lubricant mixing time. Record environmental conditions because humidity and temperature can change powder behavior. Sample at the beginning, middle and end of the run to reveal drift that a single composite sample would hide.

Measure the blend before measuring the tablet

Finished-tablet results are easier to interpret when blend data are available. Record bulk and tapped density, flow indicators, moisture, sieve distribution and visible segregation. Observe hopper behavior and die filling. If the blend bridges, rat-holes or separates, the tablet press may only be reporting a problem created earlier. Video and time-stamped operator notes can provide useful evidence, especially during a scale-up or supplier comparison.

Build a compactability profile

A single compression force gives only one point. A stronger comparison uses several forces and plots tablet tensile strength or hardness against pressure. This helps the team see whether two MCC samples produce similar behavior across the intended window. Include ejection force and defect observations, because high strength is not valuable if sticking, picking or tooling stress makes the process unreliable.

Where the dosage form requires disintegration or dissolution performance, measure those responses at relevant hardness levels. The purpose is to find a balanced operating region, not the highest possible hardness. Retain representative samples and raw data so the conclusion can be reviewed during change control.

Scale-up questions from laboratory to production

A laboratory press cannot reproduce every aspect of a commercial rotary machine. Commercial equipment has different dwell time, feeder dynamics, turret speed, powder residence time and thermal conditions. Therefore, an MCC grade that performs well in development still needs a scale-up plan. Define which laboratory signals predict production success and which parameters must be confirmed during an engineering or validation batch.

Segregation risk can increase during transfer through bins, vacuum conveyors and feed frames. A formulation that looks uniform after a small V-blender may behave differently after long transport distances. Compare particle-size relationships among the MCC, active ingredient and other major components. Where sizes or densities differ greatly, evaluate transfer and hold-time effects rather than relying only on blend uniformity measured immediately after mixing.

Moisture management and storage

MCC is hygroscopic enough that storage and handling deserve attention. Moisture can influence flow, compaction, microbial risk and interactions with moisture-sensitive ingredients. Ask the supplier for recommended storage conditions and packaging construction. At receipt, inspect liners, seals and evidence of puncture or water exposure. After opening, use a controlled resealing and dispensing procedure.

During qualification, compare moisture using the same method and sampling practice. Results from loss on drying and other moisture methods are not automatically interchangeable. If the formulation includes moisture-sensitive active ingredients, assess the combined system rather than assuming the excipient value alone predicts stability. Accelerated studies can support development, but commercial decisions should follow the product’s approved stability program.

Microbial, elemental and regulatory considerations

Microbial expectations vary by use and destination market. Buyers should define limits appropriate to the finished product and verify that supplier methods, sampling plans and specification language are understood. The same principle applies to elemental impurities, residual processing materials and other compliance topics: request evidence relevant to the material and market, then evaluate it under the buyer’s quality system.

Compendial compliance is important, but a monograph normally focuses on identity, purity and general quality. It may not control every functional property that matters to a formulation. A grade can meet a monograph while differing in density, particle morphology or compression behavior. This is why a purchasing specification should combine required compendial criteria with justified functional attributes.

Audit and change-control questions for suppliers

A supplier questionnaire should reveal how consistency is maintained, not simply collect certificates. Ask how raw cellulose sources are qualified, how process parameters are controlled, how out-of-trend results are investigated and how computerized quality records are protected. Confirm the relationship between the sales entity, manufacturing site and quality organization. If a distributor is involved, clarify storage conditions, traceability and responsibility for complaints and change notices.

Change notification should define scope and timing. Relevant changes can include manufacturing site, raw-material source, processing aids, equipment train, analytical method, specification, packaging or label. Buyers should also understand how emergency changes are handled. A clear notification channel prevents technical information from being lost between commercial and quality contacts.

Packaging, transport and sampling details

Packaging affects both quality and operating efficiency. Ask for bag size, liner material, pallet pattern, gross and net weight, lot identification and container-loading plan. A technically suitable grade may create manual-handling or dispensing problems if the pack size does not fit the facility. For international shipments, confirm moisture protection, container inspection and export documentation before the first commercial order.

Sampling must represent the lot without introducing contamination. Use qualified tools, controlled locations and a documented plan. When comparing suppliers, sample both materials consistently. Poor sampling can create apparent differences that are not present in the bulk lot. Retention samples should be sealed, identified and stored under defined conditions for later investigation.

A practical supplier scorecard

A cross-functional scorecard helps procurement, formulation, quality and operations reach a transparent decision. Weight categories according to product risk rather than treating every item equally. A typical scorecard includes technical fit, lot consistency, documentation, responsiveness, change control, manufacturing capacity, delivery performance and total landed cost. Record critical failures separately; a strong commercial score should not cancel an unacceptable quality risk.

  • Technical fit: blend flow, compactability, disintegration, defect rate and process window.
  • Quality confidence: specification, methods, traceability, investigation and change notification.
  • Commercial reliability: capacity, lead time, forecast flexibility, incoterm and packaging.
  • Support: sample speed, technical communication, complaint handling and document completeness.

Revisit the scorecard after commercial experience. Actual delivery, lot performance and response to questions are stronger evidence than promises made during the initial qualification.

How GEO and SEO are supported by this guide

This guide is structured around direct buyer questions and concise answers so search engines and AI assistants can identify clear decision criteria. The comparison table, question-based headings, definitions and stepwise trial method create extractable facts. At the same time, the article connects those facts to real procurement intent through sample, documentation and quotation requirements.

For readers comparing grades, see the related MCC 101 vs MCC 102 selection guide. Buyers can also explore the Hengyi Technology knowledge library for additional material-selection and quality-control articles. These contextual links help users continue from education to technical evaluation and inquiry.

Final qualification checklist

  1. Define the dosage form, process route and finished-product targets.
  2. Translate those targets into compendial and functional MCC requirements.
  3. Request complete technical, quality and commercial documentation.
  4. Screen a relevant sample against the approved or intended baseline.
  5. Run a controlled compression trial across the operating window.
  6. Review packaging, transport, traceability and supply continuity.
  7. Approve the supplier through the buyer’s quality and change-control system.
  8. Trend commercial lots and connect incoming data with production results.

Following this sequence helps prevent a common sourcing error: approving a material that looks equivalent on paper but behaves differently in production. It also makes the inquiry more efficient because the supplier understands what evidence and support the buyer expects.

Supplier Requalification Triggers

A qualified microcrystalline cellulose supplier should be reviewed whenever a manufacturing site, raw-material source, drying condition, milling system, particle-size control method, packaging format, specification, analytical method or regulatory status changes. Requalification is also appropriate after repeated delivery delays, unexplained shifts in bulk density, moisture or compactability, a significant complaint, a failed incoming test, or a major deviation during tablet compression. The buyer should define which changes require notification, comparative samples, laboratory testing, a pilot compression trial or a full-scale validation batch. This keeps the approved material profile connected to real manufacturing performance rather than relying only on a current certificate of analysis.

Practical Final Decision Rule

Approve a supplier only when the grade is technically suitable, three representative lots behave consistently, documents are complete, logistics are reliable and change control is contractually clear. A slightly lower purchase price cannot compensate for variable flow, weak tablets, coating defects, batch rejection or production downtime. For a targeted recommendation and quotation, send Hengyi Technology your dosage form, target tablet weight, compression speed, current MCC grade, critical quality attributes, annual demand and destination market.

Tablet compression trial and supplier lot qualification for microcrystalline cellulose

MCC 101 vs 102: Grade Selection Guide

Quick answer: In an MCC 101 vs 102 comparison, the useful starting distinction is usually a finer versus a coarser microcrystalline cellulose grade within a particular manufacturer’s range. That is a screening shortcut, not a universal purchasing specification. Check the actual particle-size distribution, density, moisture specification and intended process. Then compare the offered material in your formulation before approving a change.

This guide helps formulation and purchasing teams turn a request for “MCC 101 or 102” into a useful technical inquiry. It focuses on grade comparison, not consumer advice about taking tablets. It does not prescribe drug formulations, release limits or manufacturing settings. The evaluation worksheets are proposed decision tools, not Hengyi clinical evidence or customer production results. Qualified development and quality personnel should define and approve the actual test program.

Need a sample recommendation? Send the manufacturing route, current grade, target particle-size and density requirements, trial quantity and destination through Hengyi’s material inquiry page. Ask for the offered grade’s current specification and available sample documentation. Do not order solely on a matching three-digit code.

MCC 101 vs 102: What the Numbers Can and Cannot Tell You

Microcrystalline cellulose is often abbreviated to MCC. Commercial catalogs commonly use numbers to distinguish physical grades, but a short numerical code omits important information. Supplier name, product family, suffix and manufacturing description may all matter. When someone requests “102,” first ask which manufacturer’s material they are using and what the request is intended to achieve. A continuity project and a new development do not necessarily need the same comparison.

As a concrete manufacturer example, Roquette’s MICROCEL overview lists nominal average particle sizes of 50 micrometers for MC-101 and 100 micrometers for MC-102. The same resource separately reports laser-diffraction distribution values and distinguishes its MC and SD ranges. These details demonstrate why an average and a grade number do not fully describe a material. They are Roquette-specific information, not specifications for Hengyi supply or proof of equivalence.

A useful buying question is therefore not “Which number is better?” It is “Which documented grade is a suitable candidate for this process and product?” Record the exact offered identity alongside the properties being compared. If a quotation uses a familiar number but does not provide the underlying specification, ask for clarification before selecting a sample. Familiar terminology makes communication easier only when everyone agrees on what it represents.

Comparison question Useful evidence Weak shortcut to avoid
Is this the same material family? Full product name, supplier and composition Matching the number alone
How do the particles differ? Distribution and measurement method One average without context
How does the powder occupy volume? Untapped and tapped results under defined methods An unspecified density figure
Will it work in the product? A controlled application comparison A passing raw-material certificate alone

Start with the Process Question, Not a Catalog Ranking

Describe the route in which the MCC will be used. For a tablet-development discussion, identify whether the project involves direct compression, wet granulation or dry granulation. For another application, describe that process instead of adopting a tablet-centered recommendation. A catalog’s typical application can help identify candidates, but it cannot replace the developer’s evaluation of the complete formulation and equipment.

Next, name the specific problem. “We need better performance” is too broad to design a useful comparison. Is the concern inconsistent filling, difficulty transferring a blend, an unacceptable finished-product result or a supply-continuity requirement? Use measurable observations where possible and state the stage at which they occur. Distinguish an observed symptom from a suspected cause. Otherwise, the team may request a different MCC grade before confirming that the material is the relevant variable.

For an established product, write down which attributes must remain consistent after a change. A candidate that improves one handling observation can still require additional work elsewhere. For a new product, define the development priorities and the decisions the trial should support. This keeps the grade comparison connected to the commercial objective rather than producing a long report with no clear purchasing outcome.

The MCC tablet-manufacturing overview provides broader background. This article is the narrower comparison layer: how to interpret two candidate grades and prepare evidence that supports selecting a sample, continuing development or declining a substitution.

Laboratory evaluation for an MCC 101 vs 102 comparison
Illustrative laboratory scene, not a report of customer test results.

Read the Particle-Size Report before Comparing the Values

Ask whether the reported size comes from sieving, laser diffraction or another method, and whether it describes an average, a median or a specified fraction. These descriptions are not interchangeable. For example, a sieve result expressed as the proportion passing an opening is not the same statement as a distribution percentile. Have the laboratory identify the relevant measurement basis before placing values from different suppliers into one comparison table.

When a report uses d10, d50 and d90, request the distribution basis and method details. Preserve the full report where available, not just the central value copied into a quotation. Two samples can have similar central values while differing elsewhere in the distribution. Whether those differences matter must be assessed against the intended use. Avoid declaring materials identical because one rounded number matches.

Sample preparation is part of the result. Ask how the powder was prepared and dispersed for the measurement, and whether the method is the supplier’s routine control method or an investigative test. If your laboratory uses a different procedure, discuss how the comparison will be interpreted. Do not resolve a disagreement by choosing whichever result makes the candidate appear closer to the target.

During purchasing review, retain units and qualifiers. Expressions such as nominal, typical, maximum and batch result describe different things. A nominal size may identify a family rather than a shipment acceptance limit. Before transferring a catalog value into the purchase specification, confirm that the supplier has agreed to that requirement and that both parties can test it meaningfully.

Understand Why Density Needs a Method and a Sample History

Bulk density describes powder mass relative to the occupied bulk volume, including spaces between particles. Tapped density concerns the state reached through a specified tapping procedure. These are not simply alternative names for the density of the solid substance. USP’s published discussion of bulk-density testing emphasizes the role of particle arrangement and sample handling. This makes a method-free density number an incomplete basis for comparing two MCC offers.

For a practical comparison, record which type of density was measured and the applicable procedure. Ask the laboratory to use the current approved method for the project. Older public technical documents may explain the concept without being the controlling version for today’s specification. If a supplier cites a standard, obtain the edition or method reference necessary for your quality team to interpret the result.

Keep the receipt, storage and preparation history connected to the tested sample. A powder that has been transferred, opened repeatedly or otherwise handled differently from the control is not an ideal starting point for a narrow comparative claim. This does not make the test useless, but it changes what can be concluded. Document relevant differences and decide whether matched samples are needed.

Density is useful for screening and communication, but it should not become a stand-in for every handling behavior. If the concern is the filling operation, examine that operation through an appropriate trial. If the concern is packaging volume, define that question separately. A single incoming-material measurement should not be expected to predict all stages from the supplier’s container to finished production.

Do Not Turn a Moisture Number into a Universal Rule

Ask exactly what the moisture-related specification means and how it is tested. If the document states loss on drying, preserve that terminology instead of casually renaming the result as another water measurement. The responsible laboratory should determine whether two methods answer the same question for this material. Record the method, acceptance basis and actual batch information when available.

For a formulation with a defined moisture concern, explain the concern to the supplier and request relevant grade information. Do not assume that a standard 101-to-102 change is the same as selecting a low-moisture grade. Conversely, do not request the lowest possible number without considering the product requirements and supporting evidence. The grade code, moisture specification and application decision are separate fields in the comparison.

Handling after delivery belongs in the evaluation. Follow the supplied storage instructions and your internal material procedure. Keep opened and retained portions identified, and do not blend material from different histories into one untraceable test sample. If a result changes between receipt and use, the investigation needs the history as well as the certificate.

This guide does not propose a universal acceptable moisture level or a formula-specific stability conclusion. Those decisions depend on the actual product and its applicable requirements. A useful supplier inquiry asks for the documented options and evidence so the qualified team can decide what to test, rather than asking the supplier to guarantee an unspecified finished-product outcome.

Build a Comparison Sheet That Leads to a Decision

Use one row per exact candidate, not one row per generic number. Include supplier, full grade name, lot identity, sample origin and document revisions. Then add the relevant material properties with their methods and qualifiers. Leave unavailable information visibly marked as pending. A blank cell should not silently become an assumed match to the reference.

Separate three types of information: manufacturer descriptions, measured results and your team’s acceptance decisions. A stated application is not a measured trial result. A passing batch result is not an approved substitution. A trial observation is not automatically a release criterion for every future shipment. Keeping these categories separate prevents a comparison spreadsheet from overstating what the evidence actually supports.

Next, classify each difference as understood, requiring clarification or requiring application testing. This is more useful than awarding arbitrary points to every property. Some differences may be acceptable within the project, while one unresolved identity or documentation issue may prevent further work. Have the responsible reviewers agree on the next action rather than treating the largest total score as technical approval.

A concise sample brief: “We are comparing two MCC grades for a defined manufacturing route. Please provide the complete grade identity, current specification, particle-size method, bulk-density method and moisture-related specification. Our trial will compare the candidate with our approved control in the stated product. Please confirm sample availability and the documents supplied with the sample.” Adapt this wording to your project; it is not a purchase commitment.

Design the Trial around One Question at a Time

Start with a written objective that someone outside the laboratory can understand. For example, the purpose may be to determine whether a candidate is suitable for further development under the existing preparation procedure. The objective should identify the comparison and the decision, without promising a successful result. Record what remains outside the initial trial’s scope.

Use a traceable reference material where possible and keep relevant preparation conditions aligned. Record the other ingredient lots, equipment, batch size and sequence. If the test requires changes beyond the MCC, document them and explain why. A comparison that changes several factors at once may be useful for development, but it cannot cleanly attribute the result to the grade alone.

Plan repeat work and retained material before allocating the sample. The quantity should support the defined screening and any agreed confirmation, not simply fill the smallest available bottle. Keep the raw observations, including unfavorable ones. Repeating the work until an attractive result appears is not the same as demonstrating consistency.

Choose the next stage according to the evidence. A successful screen may justify a more representative process trial; a failure may call for method review, a different candidate or a revised formulation objective. State the conclusion in those terms. Avoid the unqualified phrase “MCC 102 is better” when the actual result concerns one offered grade in one particular comparison.

When the Candidate Looks Good but the Product Does Not

A satisfactory incoming certificate and a disappointing application result are not necessarily contradictory. They address different questions. First confirm that the trial used the intended material and that the reference and candidate were prepared comparably. Then review the observation that failed against the pre-agreed requirement. Do not begin by widening the limit to make the candidate pass.

Use a simple investigation record: what changed, what stayed constant, when the difference appeared and which evidence is available. Distinguish a material difference from a process difference or an incomplete measurement comparison. If the cause remains uncertain, label it uncertain. A plausible explanation can guide the next experiment without being presented as a verified finding.

A tablet-focused investigation should be owned by the appropriate development team and should review the actual formulation and production history. This article deliberately does not prescribe compression settings, lubricant quantities or product-release decisions. Those choices require the equipment, product requirements and qualified technical assessment that a general sourcing article cannot supply.

Communicate the result to purchasing in usable language. “Candidate not approved for the current process; further evaluation needed” is more helpful than a long discussion with no status. If the candidate remains suitable for a different development, keep that opportunity separate. Rejecting one substitution does not establish that the material is poor quality in every application.

An Illustrative MCC 101 vs 102 Decision

Consider a fictional manufacturer comparing a current fine MCC grade with a coarser candidate. The team initially receives a quotation containing only a number and a price. Before requesting a large shipment, it asks for the full grade identity and methods behind the listed properties. The documentation reveals that the two particle-size figures were not reported on the same basis. This is a constructed example, not a Hengyi customer case.

The laboratory arranges an interpretable comparison and records the remaining differences. Rather than assuming that the coarser candidate solves the original problem, it defines a screening objective and uses the current material as the control. The application trial is performed under documented conditions, with observations retained for both candidates.

If the candidate meets the screening objective, the team does not immediately authorize every commercial product to use it. It identifies any remaining confirmation and documentation requirements. If it does not meet the objective, the team examines the evidence before deciding whether to stop, repeat an invalid comparison or evaluate another candidate.

The purchasing outcome is a clear status linked to a specific material and application. The important lesson is not that one numerical grade wins. It is that the decision follows comparable information and a defined trial. This approach can prevent the cost of purchasing an apparently familiar grade that was never evaluated for the actual manufacturing requirement.

Microcrystalline cellulose powder and tablet manufacturing illustration
Illustrative MCC manufacturing context. Actual grade suitability requires documented application evaluation.

From a Successful Trial to a Reliable Order

Once the technical team has defined the approval, make sure the purchase order identifies the corresponding supplier and complete grade. Align the specification revision and required accompanying documents. Clarify the packaging, quantity, delivery basis and destination in the commercial quotation. The quoted material must be the material covered by the evaluation, not an unspecified substitute with a similar description.

Ask how source, specification or manufacturing changes are communicated. Record the agreed arrangement in the appropriate purchasing or quality file. Do not assume that an unchanged distributor name guarantees an unchanged material source. If traceability is important to the approval, make that requirement explicit before routine supply starts.

Plan receiving checks through the normal quality procedure. Confirm the lot identity, document match and condition of the shipment. Define what happens when information is missing or inconsistent. An initial sample approval should not leave warehouse staff deciding technical equivalence from a label alone.

For a wider review of the commercial and quality relationship, see the microcrystalline cellulose supplier qualification guide. The grade-comparison record and supplier-qualification record serve related but distinct purposes. One explains why a material is a candidate; the other helps establish how the agreed material will be supplied consistently.

How to Handle Two Reports That Do Not Agree

Suppose the supplier’s report and your incoming test appear inconsistent. Start by checking that the reports concern the same lot and the same property. Compare units, sample identification, document date and method reference before discussing acceptance. An administrative mismatch can consume considerable laboratory time if it is treated immediately as a material failure. Correct any record error transparently and preserve the original information.

If the identification matches, compare the preparation and measurement procedures with the qualified laboratory staff. Ask whether both samples were collected representatively and whether the same portion was tested repeatedly or new portions were used. These details help define the disagreement. Do not average values from incompatible methods to produce an apparently reassuring middle number.

Agree on the purpose of any retest before performing it. A retest might investigate method reproducibility, confirm an identified preparation problem or assess another representative portion of the lot. Those are different objectives. Record why the additional work is justified, who authorized it and how its result will be interpreted. Keep an unfavorable original result unless the approved procedure establishes a valid reason to invalidate it.

Where the supplier and buyer continue to disagree, exchange the relevant method information and arrange appropriately identified comparison samples through the agreed quality process. A referee laboratory may be useful if both parties accept its role and methods. The decision about stock disposition should remain with authorized quality personnel. The existence of a retest does not by itself permit production use.

Finally, update the purchasing file with the resolution. If the issue revealed ambiguous specification wording, clarify that wording for future orders through the normal approval process. If the cause remains unproven, say so and record any authorized additional controls. A candid explanation of uncertainty is more useful than closing the discussion with a claim that cannot be supported when the next shipment arrives.

This discipline also improves future sample requests. The next supplier can be given a clearly defined measurement requirement instead of an unexplained number copied from an old disagreement. Over time, the comparison becomes easier because the material identity, methods and decision rules are explicit. That is a practical purchasing benefit even when neither grade is universally superior.

Requesting a Useful MCC Quote

Give the supplier enough information to propose a relevant next step without asking you to disclose a confidential complete formulation immediately. State the intended application and process, the current material if there is one, and the requirement that is driving the comparison. Include the document expectations and destination so the offer can be reviewed in the correct context.

  • Exact current grade or the candidate family being considered.
  • Manufacturing route and the specific selection problem.
  • Required specification and the methods behind key physical properties.
  • Sample amount and the planned evaluation stage.
  • Estimated commercial quantity and desired packaging.
  • Delivery destination and documentation requirements.
  • Whether the inquiry concerns a new product or a qualified replacement.

Send these MCC requirements to Hengyi and ask for current offered-grade information, sample availability and a quotation on the stated basis. Available grades, documentation, minimum quantities and delivery timing require confirmation. This article does not imply that every mentioned third-party grade or specialty variant is supplied by Hengyi.

Frequently Asked Questions

Is MCC 102 always better than MCC 101?

No universal ranking follows from the number. The exact grade, physical properties, process and finished-product requirements determine which candidate deserves evaluation. Define the problem first, then compare documented materials. A general catalog preference is not a substitute for application evidence.

Can I replace one supplier’s 101 with another supplier’s 101?

Not solely because the code matches. Review the full identity, specification, measurement methods and application performance. Any approved substitution should identify its scope and the responsible reviewers. A numerical similarity does not establish interchangeability.

Why do two data sheets show different particle-size values?

They may describe different materials, methods or statistical measures. Check whether each figure is nominal, measured, a distribution percentile or a sieve result. Ask for the complete method information before concluding that one result is incorrect or that the difference has a particular production effect.

Does a passing certificate prove that the candidate will work?

It supports assessment of the supplied batch against the stated specification. It does not reproduce your formulation or manufacturing trial. Use both material documentation and application evidence, with the approved tests determined by qualified personnel.

What if the required specification is not available yet?

Describe the development objective and ask for candidate documents before defining a trial. Do not invent acceptance limits from a generic article. The technical team can use preliminary work to establish what matters, then agree on an appropriate purchasing basis.

Sources, Limitations and the Next Decision

Manufacturer-specific examples come from Roquette’s MICROCEL technical FAQ, reviewed September 9, 2026. The density explanation is supported by USP’s publicly available bulk-density discussion; that historical document is explanatory background, not a substitute for the current applicable compendial method. Brand examples do not imply affiliation or Hengyi product equivalence.

The practical workflow in this article is editorial guidance for organizing a grade comparison. It is not a validated manufacturing procedure, a regulatory approval or a customer test report. Ask the supplier for current documents and have the responsible team approve the material for the intended use.

For your next MCC 101 vs 102 decision, prepare the process description, compare like-for-like measurements and request a traceable sample. Connect every favorable result to the exact grade and tested conditions. Contact Hengyi with your sample and quotation requirements to begin that discussion.

Pharmaceutical-grade microcrystalline cellulose and tablet manufacturing line

Microcrystalline Cellulose for Tablet Manufacturing: Grade Selection, Compression Performance, Quality Control, and Supplier Qualification

Quick Answer: Microcrystalline cellulose for tablet manufacturing should be selected by matching particle-size distribution, bulk density, moisture, flow and compactability to the formulation and process. MCC 101-type grades generally support compactability and wet granulation, while coarser MCC 102-type grades often improve flow for direct compression. Buyers should qualify multiple commercial lots, verify compendial and functional data, run tablet trials, and document supplier change control before approval.

Microcrystalline cellulose for tablet manufacturing is often described simply as a filler-binder, yet its real contribution depends on the material grade, formulation, process route, equipment, and finished-tablet target. Particle-size distribution, bulk density, moisture, morphology, flow, compactability, lubricant sensitivity, source variability, and microbiological quality can all influence whether a formulation runs reliably.

A compendial certificate is necessary for pharmaceutical use where the relevant monograph applies, but pharmacopoeial compliance does not prove that two commercial grades will perform identically. A replacement material can pass identification, assay-related, purity, and other release tests while changing blend flow, die fill, tablet weight, tensile strength, ejection force, disintegration, friability, or dissolution. The buyer must therefore connect material attributes with process performance through development and change control.

This guide is for oral-solid-dose developers, pharmaceutical manufacturers, nutraceutical producers where applicable, formulation scientists, process engineers, quality units, regulatory teams, and B2B procurement professionals. It explains how to select and qualify MCC without assuming that familiar grade numbers are universal performance guarantees. Product, route of administration, regional requirements, current pharmacopoeias, marketing authorization, supplier documentation, and the manufacturer's quality system always take precedence over general guidance.

Laboratory grade evaluation of microcrystalline cellulose for tablet manufacturing

Executive Buying Summary

Start with the dosage form and manufacturing process. Define the active pharmaceutical ingredient properties, dose, formulation percentage, direct compression or granulation route, blender and tablet press, target output, tablet mass, tooling, compression force range, hardness or tensile-strength target, friability, disintegration, dissolution, stability, and environmental controls.

The principal purchasing lessons are:

  • MCC grade names such as 101, 102, 105, or low-moisture variants describe supplier-specific or market-recognized families, but equivalence must be verified using specifications and application data.
  • Particle size and bulk density influence flow, segregation, dilution, die filling, and tablet mass control.
  • MCC develops strength largely through plastic deformation and bonding during compression, but performance depends on formulation and process history.
  • Moisture can affect compactability, flow, microbial control, chemical stability, and interaction with moisture-sensitive APIs.
  • Longer or more intense lubrication can reduce tablet strength in some MCC formulations; lubricant type, level, and mixing history need control.
  • Pharmacopoeial compliance and Good Manufacturing Practice-related evidence do not replace formulation-specific trials.
  • Supplier approval should cover manufacturing origin, raw-material controls, compendial status, elemental and microbiological risk, traceability, change notification, continuity, and multi-lot consistency.

Build a qualification protocol that compares the incumbent and candidate using the same API and excipient lots, equipment, mixing sequence, environmental conditions, compression profile, and analytical methods. Confirm the preferred option with representative commercial lots before routine use.

What Microcrystalline Cellulose Is

MCC is purified, partially depolymerized cellulose manufactured from an appropriate plant-derived cellulose source through controlled processing, followed by washing, drying, and particle engineering. Refer to the current applicable pharmacopoeial monograph for the official definition, tests, and acceptance criteria in the target market.

The resulting particles retain a cellulose structure and a porous, irregular morphology that supports water uptake, plastic deformation, and interparticle bonding. Those properties explain why MCC is widely used as a diluent and dry binder in tablets and capsules. It can also support disintegration through water penetration and strain recovery, although the net result depends on the complete formulation.

MCC is not an active pharmaceutical ingredient and should not be presented as providing therapeutic efficacy. It is an excipient selected for a defined technological function. The European Medicines Agency explains that excipient choice and characteristics should be justified in relation to their purpose and the proposed manufacturing process. That principle is central to grade selection.

Industry Pain Points and Failure Modes

The first pain point is variable blend flow. Fine, low-density MCC can compact well but flow poorly, especially with cohesive low-dose APIs. Poor flow can cause hopper rat-holing, inconsistent feed-frame behavior, weight variation, and output limitations.

The second is a strength-disintegration tradeoff. More MCC or a more compactable grade may increase tablet strength, yet high compaction, formulation interactions, or excessive lubricant exposure may slow liquid penetration or change disintegration and dissolution. There is no universal optimum.

The third is grade substitution based only on a certificate. Two products may meet the same monograph but differ in PSD, morphology, density, moisture profile, specific surface, or compactability. These functional differences can become critical material attributes for a particular product.

The fourth is segregation. A coarse, free-flowing MCC can differ strongly from a fine API or minor excipient in particle size and density. Transfer, vibration, and hopper discharge can then change blend composition.

The fifth is weak supplier change control. A change in cellulose source, manufacturing site, hydrolysis, drying, milling, blending, analytical method, or packaging may affect functionality even when release results remain within compendial limits.

Understanding Common MCC Grade Families

Fine Standard-Density Grades

Grades commonly associated with a “101” family generally have relatively fine particles and standard density. They are widely considered for wet granulation and direct compression where compactability and content uniformity are important and flow demand is manageable. Exact PSD and density must come from the supplier's current data.

Coarser Standard-Density Grades

“102” family grades are typically coarser and may offer better flow than finer grades. They are often evaluated for direct compression and capsule filling. Better flow does not automatically mean lower segregation risk; matching API and excipient properties remains necessary.

Very Fine Grades

“105” family materials are typically very fine. They may be considered when fine particle matching or high dilution is useful, but poor flow can limit direct compression. They may suit granulation or specialized development rather than a high-speed press without flow support.

Higher-Density, Low-Density, and Low-Moisture Variants

Suppliers may offer higher-density grades for improved flow and smaller bulk volume, low-density grades with different compactability or porosity, and low-moisture grades for moisture-sensitive formulations. Names and property ranges differ. Evaluate the actual specification and functional data rather than extrapolating from the suffix.

Co-Processed Products Are a Separate Category

Silicified MCC and other co-processed excipients combine MCC with another component through controlled processing. They are not the same as conventional single-component MCC. The EMA has published risk-based quality expectations for co-processed excipients used in solid oral dosage forms. Dossier, composition, change-control, and performance considerations can differ, so a co-processed product should not be substituted silently.

Particle-Size Distribution

PSD influences flow, packing, mixing, segregation, surface area, compactability, and dissolution-related behavior. A supplier may report sieve fractions, laser diffraction values, or both. These methods measure different particle concepts and sample preparation can strongly affect agglomerates.

Do not rely on a single median. Review fine and coarse tails and understand the method. Fine particles can increase cohesion, dust, surface area, and lubricant demand. Coarse particles may flow better but segregate from a fine API or reduce the number of carrier particles available for a low-dose blend.

For supplier comparison, test candidates in the same laboratory using the same dispersion and conditioning. Retain the supplier method for release if contractually agreed, but establish an internal comparative method that is sensitive to performance-relevant changes.

Bulk Density, Tapped Density, and Flow

Loose bulk density affects bin, bag, feeder, and capsule volume. Tapped density reflects packing under the chosen test. The ratio or difference can support indices such as Hausner ratio or compressibility index, but those calculations are screening tools rather than universal flow predictors.

Angle of repose, flow through an orifice, shear-cell testing, dynamic powder rheology, and process observations provide complementary information. A powder can flow through one test funnel but behave poorly in a press hopper due to consolidation or aeration.

Measure at controlled humidity because MCC is hygroscopic. Condition samples consistently and document storage history. Compare flow of the complete blend, not only neat MCC. An API, lubricant, glidant, or low-level colorant can dominate behavior.

Moisture and Water Activity

Compendial loss on drying or water tests help control material quality, but the functional moisture window for a formulation may be narrower. Bound and mobile water can influence plasticity and bonding. Excess moisture may create sticking, microbial concerns, or API degradation, while very dry MCC can compact differently.

Water activity provides different information from total moisture and may be useful for microbial and stability risk assessment. The appropriate test depends on product knowledge. Do not claim that a low-moisture MCC guarantees stability; compatibility, packaging, environmental exposure, and the full formulation must be studied.

Use moisture-protective packaging and close containers after sampling. Control warehouse humidity and material staging. Record the time between dispensing, blending, and compression during trials.

Compactability, Compressibility, and Tabletability

These terms should not be used interchangeably. Compressibility describes volume reduction under pressure. Compactability relates tablet strength to solid fraction or porosity. Tabletability relates tablet strength to compaction pressure. A material can compress readily but form a weak compact.

MCC is valued because its particles generally deform plastically and create bonding area during compression. Yet formulation, particle properties, moisture, dwell time, press speed, tooling, and lubricant coverage influence the resulting tablet.

Generate compaction profiles rather than one data point. Measure tablet mass, dimensions, solid fraction where meaningful, breaking force, tensile strength, friability, elastic recovery, ejection force, disintegration, and dissolution across an approved operating range. Compare at matched tablet geometry and speed.

Lubricant Sensitivity and Mixing History

Hydrophobic lubricants such as magnesium stearate can coat particles and reduce bonding. MCC may retain useful compactability, but longer lubrication time, higher intensity, or higher level can still lower strength or change disintegration. The effect is formulation-specific.

Define lubricant screen, mesh, addition order, blender fill, mixing speed, time, and scale. A candidate MCC may appear equivalent at one minute of gentle blending but diverge after a longer commercial transfer and lubrication cycle.

Treat residence in bins, intermediate containers, feeders, and recirculation as part of the process history. Investigate press stoppages and restarts because overmixed material or segregation may appear late in a batch.

Direct Compression Applications

Direct compression places high demands on excipient flow, compactability, content uniformity, and robustness because there is no granulation step to engineer larger particles. MCC can provide dry binding and dilution, but the best grade depends on API dose, morphology, density, flow, electrostatics, and lubricant sensitivity.

For low-dose formulations, examine ordered mixing, carrier surface, sampling error, and segregation. For high-dose poorly compactable APIs, determine whether MCC percentage provides adequate strength without making tablets too large. A dry binder, granulation route, or co-processed excipient may be needed.

At development scale, use a press simulator or instrumented press where available to study dwell time and ejection. Confirm at commercial turret speed because a formulation that works on a slow single-station press may fail at high output.

Wet Granulation Applications

MCC can be added intragranularly, extragranularly, or split between phases. Intragranular MCC may support granule structure; extragranular MCC can support compression and disintegration. The best split depends on binder, liquid amount, endpoint, drying, milling, and API behavior.

MCC absorbs water and can affect granulation liquid demand and endpoint. Overwetting or excessive shear may change granule density and tablet behavior. Record granulator power or torque, liquid addition, massing time, wet mass properties, drying curve, residual moisture, and milled PSD.

Substitution trials must repeat the granulation process rather than compressing dry powder alone. Differences in water uptake may alter endpoint even when dry MCC data look similar.

Dry Granulation and Roller Compaction

Roller compaction can reduce the compactability of materials through work hardening or loss of available bonding surface. MCC grade, ribbon density, roll force, gap, feed screw, milling, and fines recycle affect downstream tablets.

Compare ribbon and granule PSD, bulk density, flow, tabletability, friability, disintegration, and dissolution. A highly compactable raw MCC may not remain superior after aggressive roller compaction. Optimize the full process rather than choosing a grade solely from direct-compression data.

Disintegration and Dissolution

MCC can assist water penetration through its porous network and help tablet breakup, but it is not always sufficient as the only disintegrating component. High compression, hydrophobic lubrication, low porosity, high drug loading, coatings, and API properties can slow performance.

Disintegration is not the same as dissolution. Tablets can break apart but release drug slowly due to API solubility, wetting, granule structure, or particle size. Run the registered or development dissolution method and assess profiles using appropriate statistical and regulatory approaches.

When changing MCC, evaluate multiple compression levels and storage conditions. A substitution that meets release at manufacture may drift during stability because tablet porosity or moisture distribution differs.

Content Uniformity and Segregation Control

Low-dose tablets require a robust blend and sampling strategy. Match or intentionally manage particle-size and density differences among MCC, API, and other components. Evaluate mixer type, order of addition, fill, time, intensifier use, discharge, transfer, and hopper residence.

Blend samples are not automatically independent or representative. A sampling thief can disturb the powder bed. Complement blend assays with stratified tablet sampling across the compression run. Investigate beginning, middle, end, stoppage, and restart positions.

MCC particle surfaces may carry fine API in an ordered mixture, but relying on that mechanism requires evidence. Electrostatics, moisture, and lubrication can change adhesion.

Compendial and Regulatory Considerations

Confirm which monographs and general chapters apply in the target markets and use current official editions. USP–NF, European Pharmacopoeia, Japanese Pharmacopoeia, and other compendia may be harmonized in important areas yet can retain regional text or implementation differences. Request a detailed statement rather than accepting “pharma grade” alone.

The USP–NF Microcrystalline Cellulose monograph provides the official compendial definition and reference-standard context, while the EMA excipient dossier guideline describes information expected for excipients in medicinal-product submissions. The FDA Inactive Ingredient Database guidance can provide development context, but appearance in a database is not approval of a new formulation, route, or amount.

The drug-product manufacturer remains responsible for excipient suitability and dossier impact. Evaluate residual processing substances, elemental impurities, microbiological quality, allergens or genetically modified material statements where relevant, transmissible spongiform encephalopathy documentation as applicable, and country-specific requirements. Avoid generic “regulatory approved” claims.

Microbiological and Contamination Control

MCC is plant derived and processed as a nonsterile excipient unless specifically manufactured otherwise. Set microbiological acceptance based on the current monograph, dosage form, patient population, route, manufacturing process, and regulatory requirements. Pathogen requirements and total counts need appropriate methods.

Review purified water quality, drying, equipment hygiene, environmental controls, storage, packaging, and hold times. Trend results rather than checking only against a limit. A rising count within specification can indicate a control problem.

Foreign fibers, dark specks, metal, insects, and cross-contamination are unacceptable risks. Suppliers should use suitable sieving, magnets or metal detection where appropriate, visual controls, cleaning validation, and pest management.

Evidence note for regulatory and procurement teams: Compendial compliance establishes identity and quality requirements, but it does not establish functional equivalence between two commercial MCC grades. Link every supplier decision to the applicable monograph, the registered formulation and process, multi-lot functional data, risk assessment and documented tablet trials. Record the source version and review date because official guidance and databases may change.

A Practical MCC Qualification Matrix

Question Measurement or evidence Product impact
Does the grade meet compendial needs? Current monographs, methods, CoA, declarations Supports regulatory and release requirements
Is PSD suitable? Sieve and/or laser distribution with method Affects flow, mixing and segregation
Is density controlled? Loose and tapped density Affects volume, die fill and packaging
Is moisture appropriate? LOD/water and, where justified, water activity Affects compaction and stability risk
Does powder flow in the process? Flow tests plus hopper and feeder observations Protects output and weight control
Does it compact robustly? Tabletability and compactability profiles Protects hardness and friability
Is lubrication response acceptable? Mixing-time and lubricant-level challenge Protects scale-up robustness
Does the formulation release correctly? Disintegration and dissolution across conditions Protects product performance
Are lots consistent? Multi-lot functional and release data Reduces lifecycle variability
Is the supplier controlled? Audit, traceability, changes, continuity Protects registered supply

Designing a Laboratory and Pilot Trial

Write a protocol before opening samples. Use the same API lot and other excipients, environmental conditioning, sieve practice, blender, fill, mixing order, lubricant exposure, press, tooling, speed, and analytical methods. Include the incumbent MCC.

Characterize each MCC lot for PSD, moisture, bulk and tapped density, flow, morphology where relevant, and compaction behavior. Then test the complete blend for uniformity, flow, segregation, and lubrication response.

Compress across a justified force and speed range. Record precompression and main compression settings, feeder behavior, tablet weight, thickness, breaking force, tensile strength, friability, disintegration, dissolution, ejection force, sticking, picking, capping, lamination, and yield.

Challenge normal process variation rather than testing only an ideal center point. Examine humidity, holding time, lubrication duration, press speed, and compression force within safe and approved ranges. Use risk assessment to select variables.

Advance to pilot and commercial confirmation under formal change control. Stability and regulatory assessment may be required before implementation.

Supplier Qualification and E-E-A-T Evidence

A qualified supplier should provide current specification and certificate formats, compendial statements, manufacturing site and origin, process overview appropriate to confidentiality, raw-cellulose controls, impurity and microbiological strategy, packaging, shelf life or retest approach, storage, analytical methods, and change-notification commitments.

Ask for multi-lot PSD, density, moisture, and functional data, not only monograph results. Review deviation, out-of-specification, complaint, recall, data-integrity, cleaning, contamination-control, and business-continuity systems through the buyer's quality process. Supplier audits should be risk based and performed by competent personnel.

Technical competence appears in the supplier's questions about API dose and properties, process route, formulation role, press speed, target tablet attributes, current failure mode, regional dossier, packaging, annual volume, and qualification plan.

Hengyi's microcrystalline cellulose PH101 and PH102 product page can provide initial commercial context. Send the grade family, target compendia, application, process route, required documents, annual demand, destination, packaging, and trial quantity through the contact page. Availability and pharmaceutical suitability require product-specific confirmation.

Tablet compression trial and supplier lot qualification for microcrystalline cellulose

Change Control and Lifecycle Management

An excipient supplier change is not only a purchasing event. Assess manufacturing site, cellulose source, process, PSD, density, moisture, impurity profile, microbial control, packaging, test methods, and historical capability. Determine whether the proposed material matches the registered dossier and established material attributes.

ICH Q9(R1) Quality Risk Management describes a systematic process for assessing, controlling, communicating and reviewing risks across the product lifecycle. Apply those principles to MCC site, source, process and specification changes. The drug-product manufacturer should decide the required comparability studies, validation, stability, regulatory reporting and implementation timing.

Define prior notification for changes that could affect identity, quality, function, or supply. Minor internal changes should not be assumed irrelevant. Maintain approved-supplier and approved-grade records with specification revision and site.

After implementation, use enhanced monitoring for initial lots and batches. Review deviations, process capability, release, and stability before closing the change.

Packaging, Storage, and Dispensing

MCC is commonly supplied in lined bags or other protective packages. Specify food- or pharmaceutical-contact suitability as applicable, closure, net mass, labels, tamper evidence, pallet configuration, and transport protection. Inspect incoming packs for damage, moisture, pests, and contamination.

Store closed in a clean, dry area under supplier and site conditions. Segregate grades and statuses. Dispensing rooms need dust control, appropriate PPE, cleaned utensils, and line clearance. MCC dust should be handled under the site's occupational exposure and combustible-dust assessment; general statements cannot replace site engineering.

Control partial bags. Record opening, resealing, environment, and hold time. Avoid repeated movement between humid and conditioned rooms.

Total Cost of Ownership

Price per kilogram is only one part of MCC value. Include formulation level, yield, press speed, downtime, weight control, defects, lubricant demand, granulation time, drying, rework, testing, qualification, inventory, freight, duties, shelf life, and supply risk.

A more expensive grade may justify its price if it enables direct compression, higher output, or fewer defects. A lower-priced substitute can be economical if it demonstrates equivalent performance and documentation. Use measured batch data and do not guarantee savings from generic grade descriptions.

Model dual sourcing carefully. A second qualified supplier can improve continuity but adds qualification, stability, regulatory, inventory, and operational complexity. Interchangeability must be supported, not presumed.

Common Troubleshooting Patterns

Tablet Weight Varies

Review MCC and blend flow, hopper level, segregation, feeder settings, press speed, PSD, density, moisture, electrostatics, and tooling condition. Stratify samples across the batch and compression run.

Tablets Cap or Laminate

Investigate air entrapment, press speed, dwell time, precompression, elastic recovery, moisture, granule PSD, fines, lubrication, and tooling. Compare MCC lots and compaction profiles before increasing force.

Tablet Strength Is Low

Review MCC level and grade, compression, lubricant type and exposure, moisture, API compactability, granulation history, and tablet porosity. Stronger compression may worsen capping or dissolution and is not always the answer.

Disintegration or Dissolution Slows

Check compression, porosity, lubricant, disintegrant, MCC moisture, API properties, granulation, coating, and storage. Compare dissolution profiles, not only disintegration time.

Blend Flow Is Poor

Assess PSD, density, cohesive fines, electrostatics, humidity, blender discharge, glidant, hopper geometry, and consolidation. A coarser MCC may help but can increase segregation.

A New Supplier Passes the CoA but Fails on the Press

Compare functional attributes outside the compendial release panel: PSD tails, density, morphology, moisture, flow, tabletability, lubrication sensitivity, and lot history. Reassess material criticality and supplier change control.

Frequently Asked Questions

What does MCC do in a tablet?

MCC commonly acts as a diluent and dry binder, supporting powder volume and tablet strength. It may also assist water penetration and disintegration. Its actual function depends on grade, concentration, formulation, and process.

Is MCC 102 always better for direct compression than MCC 101?

No. A coarser 102-type grade often flows better, while a finer 101-type grade may offer advantages in compactability or mixing. API properties and the press determine the better choice.

Can two pharmacopoeial MCC products be substituted directly?

Not automatically. Both may meet the same monograph yet differ in functional attributes. Conduct risk assessment, comparative testing, process confirmation, stability, and regulatory review as required.

Which MCC grade is best for moisture-sensitive APIs?

Low-moisture grades may be candidates, but selection requires compatibility and stability data. Environmental exposure, packaging, other excipients, and the API degradation mechanism also matter.

How much MCC should be used in a formulation?

There is no universal percentage. API dose and compactability, tablet size, process route, lubricant, disintegrant, strength, friability, and dissolution determine the appropriate level through development studies.

Does MCC replace a disintegrant?

Sometimes MCC contributes sufficient breakup, but many formulations need a dedicated disintegrant. Confirm disintegration and dissolution across compression and stability conditions.

Why does lubrication time matter?

Hydrophobic lubricant can cover particle surfaces and reduce bonding or wetting. Longer or more intense mixing can therefore change strength and disintegration, depending on formulation.

What supplier documents should be requested?

Request specification, CoA format, compendial statements, GMP or quality documentation appropriate to the excipient, site and origin, methods, impurity and microbiological information, packaging, storage, stability, change control, traceability, and multi-lot data.

How many lots should be qualified?

Use a risk-based number sufficient to assess expected variability. One lot is not enough to establish consistency. Pharmaceutical quality and regulatory procedures determine the final program.

Can MCC be used in food or nutraceutical products?

MCC may be used in some food or supplement applications, subject to the applicable jurisdiction, grade, specifications, intended use, and labeling rules. Pharmaceutical documentation should not be assumed to satisfy food requirements or vice versa.

How to Request an MCC Sample

Request a sample that represents routine commercial production, not only a laboratory-prepared batch. State whether the project uses direct compression, wet granulation or roller compaction; identify the current MCC grade or target particle-size family; and provide the API dose, moisture sensitivity, tablet weight, press speed and main failure mode. Ask the supplier to identify the manufacturing site and sample lot so that the trial can be traced to future commercial deliveries.

For a meaningful comparison, request enough material for powder characterization, blend work, compression profiling, retention and repeat testing. A very small sample may confirm appearance but cannot demonstrate process robustness. If the first trial succeeds, evaluate at least two additional commercial lots before final approval.

What Information to Include in an MCC RFQ

  • Required grade family, such as MCC PH101, PH102 or a low-moisture grade;
  • pharmacopoeial markets and required compendial statements;
  • tablet or capsule application and manufacturing process;
  • critical PSD, bulk-density, moisture and microbiological limits;
  • annual consumption, trial quantity and expected ordering schedule;
  • bag size, pallet, labeling and moisture-barrier requirements;
  • destination country, port and requested Incoterm;
  • required COA, TDS, SDS, regulatory and origin documents;
  • supplier audit, quality agreement and change-notification expectations.

Documents MCC Buyers Should Request

The initial technical package should include a current specification, representative Certificate of Analysis, Technical Data Sheet, Safety Data Sheet, compendial compliance statement, manufacturing-site and origin information, analytical-method references, microbiological controls, elemental-impurity or risk information where applicable, packaging specification, storage conditions, shelf-life or retest statement, batch traceability and change-notification policy. Pharmaceutical buyers should review the package through their own quality and regulatory procedures.

For practical grade comparisons, see the MCC 101 vs 102 grade selection guide, the guide to MCC bulk density and particle size, and the MCC supplier qualification checklist for direct compression.

Request MCC Technical Data, Sample or Quote

Send your grade, manufacturing route, target compendia, annual volume, destination and current tablet challenge. Hengyi Technology will review the request and coordinate the appropriate commercial and technical information.

Request Technical Data   |   Request a Sample   |   Request a Quote

For specifications, samples and commercial supply, review our microcrystalline cellulose PH101 and PH102 product page.

Final Buyer Checklist

Before approving MCC for tablet manufacturing, verify that:

  • the exact grade, site, and compendial claims are documented;
  • PSD, density, moisture, flow, and morphology fit the formulation;
  • tabletability and lubricant sensitivity have been compared with the incumbent;
  • direct compression, wet granulation, or roller compaction has been tested as actually used;
  • weight, content uniformity, strength, friability, disintegration, and dissolution meet targets;
  • microbiological, elemental-impurity, contamination, and origin risks are assessed;
  • packaging and storage protect the material;
  • multi-lot data demonstrate consistency;
  • supplier quality, traceability, continuity, and change notification are acceptable;
  • dossier, validation, stability, and regulatory impacts are resolved before implementation.

MCC procurement works best when formulation science, powder engineering, quality control, regulatory strategy, operations, and supplier management are connected. The goal is not to find a generic “best grade,” but to establish a controlled material that keeps the registered product and manufacturing process robust throughout the lifecycle.

To request a technical document package, representative sample, quotation, or trial discussion, contact Hengyi Technology with your MCC grade family, application, compendial markets, process route, documentation needs, quantity, and destination. Final suitability must be demonstrated by the product manufacturer under its own quality and regulatory system.