Antioxidant 1010 for polypropylene injection molding stabilization and quality control

Antioxidant 1010 for Polypropylene Injection Molding: Thermal Stability, Melt Flow, Color Control, Processing Trials and Supplier Qualification

Antioxidant 1010 for polypropylene is commonly evaluated when manufacturers need durable primary stabilization with low volatility and good processing compatibility. The correct choice cannot be made from a product name alone: purity, physical form, dispersion, additive interactions and lot consistency all influence real molding performance.

This technical guide explains how to qualify Antioxidant 1010 for polypropylene injection molding through raw-material analysis, compounding controls, melt-flow retention, oxidative-induction testing, color measurement, aging and production trials. It is intended for formulators, quality teams and purchasing specialists.

Numerical acceptance limits must be based on the intended resin, end use and applicable standards. The purpose of qualification is to create a repeatable evidence chain from supplier lot to molded-part performance, not to claim that one universal dosage or laboratory result guarantees service life.

Antioxidant 1010 for Polypropylene: Complete Qualification Framework

1. Why Polypropylene Needs Primary Antioxidant Protection

Polypropylene is vulnerable to thermo-oxidative chain scission during pellet production, compounding, injection molding and long-term service. Heat and shear create radicals, oxygen sustains the reaction, and molecular-weight loss can appear as rising melt flow, embrittlement, odor or color change.

A stabilization program must protect the resin during each heat history without compromising appearance, regulatory obligations or downstream performance. Antioxidant 1010 is widely evaluated as a high-molecular-weight hindered phenolic primary antioxidant because it can interrupt radical propagation and has low volatility under many polypropylene processing conditions.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

2. What Antioxidant 1010 Is

Antioxidant 1010 is a sterically hindered phenolic stabilizer with multiple phenolic groups on a relatively large molecule. The phenolic hydrogen is donated to reactive polymer radicals, while steric design helps produce a comparatively stable antioxidant-derived radical that does not continue rapid oxidation.

The commercial name alone is not a complete specification. Purity, melting behavior, volatile content, color, particle form, residual impurities and packaging cleanliness can vary among sources. Qualification should connect these attributes with the buyer’s polypropylene grade, additive package and molding process.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

3. Primary Antioxidant Mechanism

During oxidation, polypropylene forms alkyl, peroxy and hydroperoxide species. A primary antioxidant reacts mainly with propagating peroxy radicals and slows the chain reaction before extensive polymer damage occurs. It is consumed over time, so performance depends on concentration, dispersion and the complete thermal history.

Laboratory interpretation should distinguish processing stabilization from service-life stabilization. A formulation that preserves melt flow through one molding pass may not retain enough antioxidant for oven aging, and a high initial oxidative-induction result does not automatically predict every outdoor or chemical-exposure condition.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

4. Why High Molecular Weight Matters

A high molecular weight generally lowers volatility and reduces the tendency of the stabilizer to migrate rapidly from polypropylene. This is useful when the resin experiences elevated melt temperatures, vacuum venting, drying or prolonged service. Retention can support consistent protection after multiple processing cycles.

Low volatility does not eliminate every loss mechanism. Poor dispersion, dust extraction, adsorption onto fillers, chemical consumption and extraction by contacting media can all reduce effective concentration. A supplier comparison should therefore include polymer performance rather than relying only on molecular structure.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

5. Purity and Assay Control

Assay indicates how much of the delivered material is the intended antioxidant, but the method and reference basis matter. Chromatographic purity can reveal related substances, while functional performance reflects all components in the commercial powder or granule.

Set an assay limit with a defined analytical method and require representative lot data. Compare chromatograms during qualification, investigate new peaks and maintain reference material. A small assay difference may be less important than an impurity that affects color, odor or regulatory compliance.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

6. Melting Range and Thermal Characterization

Melting behavior supports identity confirmation and influences how the antioxidant disperses during compounding. Differential scanning calorimetry can reveal the principal transition, broadening, multiple events or unexpected thermal history. A changed profile may signal polymorph differences, contamination or degradation.

Use consistent sample mass, heating rate, atmosphere and calibration. Do not treat one DSC number as a complete release test; combine it with assay, appearance and polymer trials. Trending onset and peak values across lots can detect changes earlier than a wide pass-fail range.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

7. Volatile Matter and Moisture

Volatile content can affect feeding, storage stability, odor and process cleanliness. Although antioxidant 1010 is selected partly for low volatility, delivered powder may contain moisture or trace processing residues. Humid storage can also change flow and create agglomerates.

Define loss-on-drying conditions and distinguish water from other volatiles when necessary. Sample sealed containers, record exposure time and compare fresh and warehouse-aged material. For hygroscopic co-additives, control the complete additive blend rather than assigning every molding defect to the antioxidant.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

8. Particle Size and Feeding Consistency

Fine powder disperses quickly but may dust, bridge or separate from polypropylene pellets; coarse particles reduce dust but may feed irregularly or leave localized concentration differences when mixing is weak. Granular or masterbatch forms can improve handling at a higher conversion cost.

Measure a meaningful size distribution and observe flow through the actual loss-in-weight feeder. Validate low-dose accuracy, hopper refill behavior and blend uniformity. The best physical form is the one that produces repeatable polymer concentration under production conditions.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

9. Color, Whiteness and Initial Appearance

The stabilizer’s powder color and trace chromophores can influence natural or lightly pigmented polypropylene. Initial plaque color is also affected by resin history, catalyst residues, processing temperature, pigments and other additives, so raw-material appearance must be interpreted in context.

Measure powder color under controlled geometry and evaluate molded plaques using consistent thickness, surface finish and conditioning. Record L*, a*, b* and yellowness where appropriate. Compare both initial color and color change after heat exposure because two sources can start alike but age differently.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

Antioxidant 1010 for polypropylene thermal stability melt flow and color testing
Thermal analysis, melt-flow retention and color measurements connect antioxidant identity with polymer performance.

10. Solubility, Compatibility and Blooming Risk

Antioxidant 1010 must remain sufficiently compatible with the polypropylene matrix to provide protection without objectionable surface deposition. Compatibility depends on concentration, crystallinity, cooling rate, other additives, fillers and service temperature.

Inspect molded parts after controlled conditioning at room and elevated temperatures. Use microscopy, surface analysis or extraction when a haze is suspected. Do not assume every deposit is antioxidant; lubricants, slip agents, nucleating agents and mold-release materials can produce similar symptoms.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

11. Selecting the Addition Level

Effective concentration is application-specific. Too little antioxidant can leave the polymer vulnerable, while unnecessary excess increases cost and may affect color, migration or regulatory calculations. The optimum level depends on resin stability, melt temperature, residence time and required lifetime.

Design a dose-response study around the supplier’s recommended range and include an unstabilized or established control where safe and practical. Evaluate more than one response—melt flow, color, oxidative-induction time and aging—because the lowest dose passing one test may fail another.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

12. Synergy with Phosphite Secondary Antioxidants

Primary phenolics and phosphite secondary antioxidants often work together. The phenolic component intercepts radicals, while the phosphite decomposes hydroperoxides during processing. The combination can preserve molecular weight and color more efficiently than either component alone.

Optimize the ratio for the actual polypropylene and process. Phosphite hydrolysis, moisture, acid scavengers and pigment interactions can alter results. A new antioxidant 1010 source should be tested inside the complete package rather than as an isolated laboratory ingredient.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

13. Interaction with Acid Scavengers

Calcium stearate, hydrotalcite and related materials neutralize acidic residues and protect processing stability. Their purity, moisture and metal-ion profile can influence antioxidant consumption and color. Changing the scavenger may therefore change the apparent performance of antioxidant 1010.

Keep scavenger source and level constant in comparative trials. Monitor plate-out, odor, color and melt flow. When a formulation change improves one property but worsens another, use a structured experiment to separate chemical interaction from feeding or dispersion effects.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

14. Interaction with Pigments and Fillers

Titanium dioxide, carbon black, organic pigments, talc, calcium carbonate and glass fibers introduce surfaces and trace impurities that may adsorb or catalytically consume stabilizers. Filled polypropylene also experiences different shear, thermal conductivity and mechanical stress.

Test the antioxidant in the final colored or filled formulation whenever possible. Include pigment heat stability, filler moisture and metal contamination in the investigation. A clean natural-resin result is useful screening evidence but not a substitute for application validation.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

15. Compounding and Dispersion

Antioxidant distribution begins with accurate weighing and dry blending, then depends on screw configuration, feeding location, melt mixing and pelletization. Poor dispersion creates local under-stabilization even when the average assay is correct.

Use a premix or masterbatch when dosage accuracy requires it, and control feeder calibration and refill cycles. Sample pellets across time, measure antioxidant content or correlated performance, and inspect variance. A stable average with wide within-lot variation is not acceptable process control.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

16. Extrusion Temperature and Residence Time

Higher melt temperature accelerates oxidation and antioxidant consumption, while long residence time increases exposure. Dead zones, shutdowns and slow starts can create degraded polymer that contaminates an otherwise controlled batch.

Map barrel temperatures, melt temperature, throughput and residence-time indicators during the trial. Compare normal and challenging conditions within the intended operating window. The stabilization package should provide margin for routine variation without being used to conceal poor equipment hygiene.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

17. Melt-Flow Retention Through Multiple Passes

Melt flow rate is a practical indicator of polypropylene molecular-weight change. For typical polypropylene, oxidative chain scission often increases melt flow after repeated extrusion or molding. The exact response also depends on shear history and measurement conditions.

Run controlled multiple-pass experiments with identical equipment, temperature profile, throughput and pellet conditioning. Report absolute melt flow and percentage change, and test duplicates. A flatter trend supports processing stabilization, but it should be confirmed with color and thermal-oxidation data.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

18. Oxidative Induction Time Testing

Oxidative induction time or temperature by DSC measures how long or at what temperature oxidation accelerates under defined conditions. It is valuable for formulation comparison and quality monitoring, but results are highly method-dependent and do not directly equal field lifetime.

Specify specimen preparation, heating program, purge gases, oxygen flow, sample pan and endpoint calculation. Use the same laboratory method across sources. Interpret OIT alongside antioxidant content and aging because morphology, pigments and sample history can shift the result.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

19. Oven Aging and Embrittlement

Elevated-temperature oven aging accelerates thermo-oxidative damage and allows comparison of time to cracking, loss of tensile properties or embrittlement. It provides application-relevant evidence when specimen geometry, airflow and evaluation criteria are controlled.

Mold specimens from randomized compounds, condition them consistently and rotate positions in the oven. Record color and mechanical properties at intervals rather than only final failure. Acceleration factors should not be claimed without a validated model linking test and service conditions.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

20. Injection Molding Process Trial

A pilot molding trial reveals feeding, dispersion, odor, deposit, color and part-quality effects that small analytical tests miss. Use a representative mold and enough material to establish stable conditions after the previous resin is purged.

Lock melt and mold temperatures, injection speed, back pressure, cycle time and regrind policy. Sample parts at defined intervals and record rejects. Challenge the upper end of the approved residence time to evaluate stabilization margin while respecting safe processing limits.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

Polypropylene injection molding trial evaluating antioxidant 1010 processing stability
A controlled molding trial evaluates dispersion, color, odor, deposits and part quality under realistic processing conditions.

21. Part Appearance and Mechanical Performance

Check gloss, haze, streaks, black specks, splay, odor and dimensional consistency. Stabilization prevents degradation but cannot correct moisture, contamination or poor venting. Mechanical testing should include properties relevant to the part, such as tensile, impact or flexural response.

Compare initial results and results after heat aging. Use statistically meaningful sample numbers and randomize measurement order. When a visual difference appears, analyze resin and deposits before changing additive dosage; otherwise the team may treat the symptom rather than the source.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

22. Analytical Measurement of Antioxidant Content

HPLC and related techniques can quantify antioxidant 1010 after suitable extraction and calibration. Measuring delivered material, compounded pellets and molded parts helps distinguish dosing error, processing loss and consumption.

Validate extraction recovery for the specific polypropylene, fillers and pigments. Use internal standards or quality-control samples, define detection limits and protect extracts from degradation. Correlate concentration with melt flow and OIT to create a useful process-monitoring model.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

23. Migration, Extraction and Application Compliance

Food-contact, medical, packaging and other regulated uses require assessment against the rules and specifications applicable to the destination and end use. Overall formulation, concentration, migration, impurities and supplier documentation may all matter.

Obtain current regulatory statements and safety data, but do not treat a supplier declaration as approval of the finished article. The manufacturer must evaluate intended conditions and applicable limits with competent regulatory support. Document grade, lot and change control.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

24. Incoming Quality Control

An incoming plan may include identification, appearance, assay, melting behavior, volatiles, color and particle form. Test frequency should reflect supplier capability, process sensitivity and historical performance rather than applying the same burden to every attribute.

Use representative sampling, sealed retain samples and calibrated methods. Trend results against the approved qualification lots. A value drifting inside specification can justify early investigation when polymer performance moves in the same direction.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

25. Supplier Qualification and Total Cost

A reliable supplier controls raw materials, reaction, purification, finishing, packaging, contamination prevention and traceability. Qualification should examine analytical capability, change notification, capacity, business continuity and corrective-action discipline.

Calculate total cost through usable yield, feeder stability, compounding output, color rejects, mold cleaning, test burden and customer risk. Approve the product only after several lots and a production-scale trial, and maintain a qualified alternate source before an emergency occurs.

For qualification, convert this topic into a written test method, sampling rule and decision limit. Compare at least three representative supplier lots with the approved control, retain raw data and preserve samples. Investigate trends before they become failures, and require documented notification for changes in manufacturing site, raw materials, process or physical form. This approach improves troubleshooting, protects formulation knowledge and prevents purchasing price from being separated from production risk.

Frequently Asked Questions

Is Antioxidant 1010 a primary or secondary antioxidant?

It is a hindered phenolic primary antioxidant that interrupts radical propagation. It is often combined with a phosphite secondary antioxidant.

What dosage should be used in polypropylene?

There is no universal dosage. The optimum level depends on resin, heat history, additive package, service requirements and applicable regulatory limits.

Can Antioxidant 1010 prevent every color problem?

No. It can reduce oxidative discoloration, but catalyst residues, pigments, phosphites, moisture, contamination and excessive temperature also affect color.

Why test melt flow after multiple passes?

Repeated processing creates controlled heat and shear histories. Melt-flow change provides a practical indicator of molecular-weight degradation.

Does a higher OIT always mean a longer service life?

No. OIT is method-specific and useful for comparison, but field lifetime depends on temperature, oxygen, stress, chemicals, geometry and antioxidant depletion.

Can powder and masterbatch forms be compared directly?

They can deliver the same active ingredient, but dosing accuracy, carrier resin, dispersion, cost and contamination risk must be evaluated separately.

How many supplier lots should be qualified?

Multiple independent lots plus a production-scale trial provide stronger evidence than one sample. The exact plan should reflect application risk.

What should trigger requalification?

Changes in manufacturing site, synthesis, raw materials, finishing, particle form, packaging or significant quality trends should trigger a documented review.

Conclusion

Successful use of antioxidant 1010 for polypropylene depends on more than selecting a familiar molecule. Manufacturers should connect identity, purity, physical form and additive compatibility with compounding consistency, melt-flow retention, color, OIT, oven aging and injection-molding evidence. Multi-lot qualification, retained controls and supplier change management create the stable operating window needed for reliable parts and defensible total cost.
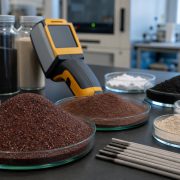
Rutile sand for welding electrode flux quality control and supplier qualification

Rutile Sand for Welding Electrode and Flux Applications: TiO2 Grade, Particle Size, Arc Stability, Slag Behavior and Supplier Qualification

Rutile sand for welding electrode flux must be qualified as more than a titanium-bearing commodity. The mineral supplies TiO2, but its particle-size distribution, associated oxides, moisture, surface condition and lot consistency determine whether an electrode coating mixes cleanly, extrudes uniformly and delivers the intended arc and slag response.

This guide gives welding-consumable formulators, purchasing teams and quality laboratories a practical framework for comparing sources. It links certificate values to manufacturing trials, welding evaluation and supplier controls so that decisions are based on repeatable evidence rather than one attractive laboratory result.

No universal rutile grade is ideal for every electrode. The correct specification depends on the total flux formula, target classification, equipment, drying schedule and customer use. Numerical limits should therefore be established through controlled trials and maintained with statistical lot data.

Rutile Sand for Welding Electrode Flux: A Qualification Framework

1. What Rutile Sand Means in Welding Consumables

Rutile sand is a naturally occurring mineral concentrate in which titanium dioxide is mainly present as rutile. In welding-consumable production it is not purchased only as a chemical source of TiO2; it is selected as a functional flux raw material that influences ionization, molten-slag properties, electrode coating behavior and the appearance of the deposited weld.

A useful qualification therefore connects mineral data with electrode or flux performance. Procurement teams should distinguish rutile sand from pigment-grade titanium dioxide, synthetic rutile and mixed titanium concentrates, because equal nominal TiO2 values do not guarantee equal particle shape, impurity pattern or welding response.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

2. Mineralogy and TiO2 Grade

The TiO2 assay is the first screening value, but mineralogical form matters. Rutile has a different crystal structure, density and thermal response from ilmenite, anatase or altered titanium minerals. A concentrate with a high total titanium result can still contain phases that change melting behavior and the chemistry of the slag.

Request total TiO2 by a validated method together with mineral-phase information when the deposit or beneficiation route is unfamiliar. Compare several production lots rather than relying on one certificate, and define whether the purchasing limit is an absolute minimum, a target range or a control band linked to the approved formula.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

3. Natural Rutile, Synthetic Rutile and Upgraded Concentrates

Natural rutile sand is mined and physically concentrated, while synthetic rutile is produced by removing iron from ilmenite-rich feed. Upgraded concentrates may sit between these descriptions. Each route creates a characteristic impurity fingerprint and particle surface that can affect binder demand, coating extrusion and high-temperature reactions.

Do not substitute one route for another solely by matching TiO2. Run a controlled formula trial at equal dry-solids basis, document any water or binder adjustment, and compare electrode manufacture as well as welding results. A technically acceptable alternate source should have written limits for both routine chemistry and process-critical properties.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

4. Particle-Size Distribution

Particle size governs packing in a coated-electrode mix, surface area exposed to binder and the rate at which rutile participates in the molten flux. Excess coarse material can create coating roughness, extrusion defects or local heterogeneity, whereas too much ultrafine material can increase water demand, dusting and batch viscosity.

Specify the distribution with more than one sieve residue or a single average. Laser diffraction can supply D10, D50 and D90 values, while wet or dry sieving remains useful for controlling oversize. The measurement method, dispersion conditions and reporting basis must stay constant because apparent differences can be created by testing technique.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

5. Particle Shape, Surface Texture and Bulk Density

Angular grains, rounded grains and porous agglomerates do not pack or wet identically. Shape affects interparticle friction during mixing and extrusion, while bulk density changes volumetric feeding and warehouse handling. Surface texture may also carry residual clay or process reagents that alter binder interaction.

Record loose and tapped bulk density, inspect representative particles by microscopy and observe flow through the actual feeder. These inexpensive checks often explain a batch that meets chemistry but behaves differently on the coating line. Supplier process changes should trigger comparison against the approved physical reference.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

6. Moisture and Drying Behavior

Moisture affects weighing accuracy, dry-mix consistency and hydrogen control. Free surface water is not the only concern; some mineral impurities or porous particles retain moisture that is released later during electrode drying or baking. Uncontrolled storage humidity can therefore erase the benefit of a good incoming specification.

Measure loss on drying under a defined temperature and time, not with an unspecified quick test. Evaluate material after transport and warehouse exposure, establish resealing rules for partial bags and use first-in-first-out inventory. Where the welding classification has strict hydrogen requirements, include the rutile source in the complete moisture-control plan.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

7. Iron Oxides and the Fe Impurity Profile

Iron-bearing phases are common companions to titanium minerals. Their oxidation state and mineral association can influence color, redox balance, slag fluidity and the amount of metallic additions needed elsewhere in the formula. A total iron number alone may not describe how that iron reacts in the arc.

Use XRF or wet chemistry for routine control and periodically confirm mineralogy when the deposit varies. Qualification trials should track arc sound, spatter, slag coverage and deposit chemistry. If a higher-iron source is accepted, the formulation response must be validated rather than corrected casually at production scale.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

8. Silica, Alumina, Zircon and Chromium Impurities

Silica and alumina participate directly in the slag network, zircon minerals add refractory behavior, and chromium-bearing contamination may introduce regulatory or metallurgical concerns. Small changes can shift melting range, viscosity and slag detachability even when the main TiO2 assay remains stable.

Set limits according to the consumable design and the sensitivity demonstrated in trials. Supplier certificates should report the same oxide basis each time, and the buyer should periodically verify results independently. Trend charts are more informative than pass-or-fail review because gradual drift can warn of a mining-face or separation change.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

Rutile sand particle size and chemical impurity testing in a quality control laboratory
Particle-size, mineral and chemical testing converts a rutile sand description into measurable incoming controls.

9. Sulfur, Phosphorus and Other Trace Elements

Sulfur and phosphorus are closely watched because excessive transfer to weld metal may reduce toughness or increase cracking sensitivity. Other trace elements can matter for a specific classification, base metal or customer requirement. Their acceptable levels should be derived from the complete formulation, not copied blindly from a generic mineral specification.

Use methods with detection limits comfortably below the purchasing limit and require transparent reporting for results below quantification. During qualification, analyze deposited weld metal under a controlled welding procedure. This links raw-material variability to the property that the customer ultimately buys.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

10. Magnetic Contamination and Metallic Foreign Matter

Mining, grinding and conveying equipment can introduce tramp iron or other metallic particles. These contaminants may disturb formula balance, create localized reactions or damage downstream equipment. Visible foreign matter also signals weak housekeeping and raises concern about less obvious contamination.

Apply magnetic separation where appropriate and include a simple magnet or microscopic inspection in incoming control. Investigate recurring findings by lot, container and supplier production date. A supplier should explain preventive maintenance, screen integrity and cleaning controls rather than only replacing a rejected shipment.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

11. Radioactivity and Responsible Documentation

Mineral sands can contain naturally occurring radioactive mineral traces, and requirements vary by origin, concentration and destination. The objective is not to assume that a rutile shipment is hazardous, but to obtain appropriate documentation and comply with applicable transport, workplace and import rules.

Ask the supplier for origin, safety data, regulatory statements and test information appropriate to the market. Qualified specialists should interpret any radiation data. Keep records linked to the lot, and avoid making compliance decisions from a marketing claim or an isolated measurement without method and unit information.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

12. Role of Rutile in Electrode Coatings and Fluxes

In rutile-type welding electrodes, TiO2-rich materials help create a readily ionized, manageable arc system and a slag that supports bead shape. Rutile works together with silicates, carbonates, ferroalloys, cellulose, iron powder and other minerals; it never acts independently of the complete recipe.

The practical purchasing question is therefore whether a particular rutile sand produces a stable process window in the buyer’s formula. Screen chemistry first, then test mixing, extrusion, drying and welding. Keep a retained sample of the approved lot so that later deliveries can be compared physically and analytically.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

13. Arc Ignition, Re-Ignition and Stability

A good rutile-based system can support easy arc starting, smooth re-ignition and a steady transfer pattern. Mineral chemistry and particle distribution influence the plasma environment and the speed of flux melting. Variability may appear as a harsh arc, wandering, intermittent extinction or sensitivity to current setting.

Evaluate performance with trained welders and, where possible, instrumented voltage and current recording. Use the same power source, polarity, electrode diameter, conditioning and base plate. Separate genuine raw-material effects from coating eccentricity, moisture, operator angle and electrical instability.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

14. Slag Formation, Viscosity and Detachability

The molten slag must cover the pool, shape the bead and then release predictably after cooling. Rutile contributes to melting and viscosity, but silica, alumina, carbonates and fluorides modify the result. A change in impurity profile can turn a balanced slag into one that is too fluid, too tenacious or uneven.

Score slag coverage, edge lift, self-peeling behavior and removal force on defined bead positions. Inspect for trapped slag and undercut rather than celebrating easy release alone. The best raw material is the one that creates a robust balance across the intended welding range.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

15. Weld Bead Appearance and Positional Performance

Customers notice bead contour, ripple regularity, toe wetting and surface cleanliness. These features are influenced by the way the coating melts and protects the pool. A rutile source that performs well in flat position may behave differently in vertical, overhead or fillet tests.

Use test joints representative of the consumable’s market, photograph beads under consistent lighting and record current, travel speed and electrode angle. Compare blind-coded samples when possible. Visual evaluation should support, not replace, dimensional measurements and defect inspection.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

16. Spatter, Fume and Operator Experience

Spatter level, arc sound, smoke behavior and slag handling affect productivity even when deposited metal passes mechanical tests. A mineral change can alter transfer smoothness or create dust during manufacturing. Operator observations are valuable when collected with a structured score sheet.

Include manufacturing staff and welders in the trial review. Measure fume or workplace exposure where required using competent industrial-hygiene methods; do not infer safety from appearance. Supplier qualification should include a current safety data sheet and clear handling guidance for mineral dust.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

17. Mechanical Properties and Hydrogen Context

Tensile strength, yield strength, elongation and impact toughness arise from weld-metal composition, cooling and soundness. Rutile sand can influence these indirectly through slag reactions and transfer of trace elements. Moisture associated with any flux ingredient also belongs in the hydrogen-risk assessment.

Prepare deposited-weld-metal tests according to the relevant consumable standard and approved procedure. Confirm chemical composition before explaining a mechanical result. If diffusible hydrogen is a requirement, control electrode manufacture, rebaking, exposure and testing conditions so that the rutile comparison is meaningful.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

Pilot welding electrode trial evaluating rutile sand arc stability and slag behavior
A controlled welding trial confirms how a candidate rutile source performs in the complete electrode formulation.

18. Balancing Rutile with Other Formula Components

Carbonates control gas and basicity, silicates provide binding and slag structure, ferroalloys adjust composition, and iron powder changes deposition rate. Increasing rutile to improve operability can shift oxygen potential, slag volume and mechanical performance. Every adjustment creates interactions.

Use designed experiments for major reformulation instead of changing one ingredient repeatedly without a model. Record each formula on a dry-mass basis and track raw-material lot numbers. The goal is a wide operating window, not a single attractive bead produced under ideal laboratory conditions.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

19. Binder Compatibility and Water Demand

Sodium or potassium silicate binders must wet the mineral blend and provide adequate green strength for extrusion. Fine or porous rutile can raise binder or water demand, while surface residues may affect setting. An apparently small adjustment can change drying stress and coating durability.

Measure mix consistency, extrusion pressure, coating adhesion and recovery after controlled storage. Fix the order of addition and mixing energy during comparative work. If a substitute rutile requires a different binder ratio, verify that this change does not compromise arc behavior, moisture resistance or shelf stability.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

20. Mixing, Extrusion and Electrode Drying

Production suitability begins before welding. The mix should distribute uniformly, feed without segregation and extrude as a concentric coating. Drying must remove water without cracks, blisters or loss of adhesion. Particle distribution and mineral contaminants can influence every stage.

Run enough pilot material to reach steady equipment conditions and examine electrodes from start, middle and end of the batch. Record extrusion pressure, scrap, eccentricity and drying defects. A lower mineral price can be eliminated quickly by slower output or increased rejection.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

21. Designing a Laboratory Electrode Trial

Begin with a control made from the currently approved rutile and a test batch differing only in rutile source. Use calibrated scales, documented moisture corrections and identical mixing and drying schedules. Make enough electrodes for process evaluation, welding tests and retained samples.

Blind-code the electrodes if practical. Conduct a screening round, then repeat promising results on a separate day or batch. Define acceptance criteria before seeing results, including manufacture, arc behavior, slag, appearance, weld-metal chemistry and required mechanical properties.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

22. Controlling the Welding Procedure

Welding comparisons fail when current, voltage, polarity, electrode conditioning, base material or welder technique changes. A detailed test sheet should capture machine identification, ambient conditions, joint geometry, run sequence and electrode exposure time.

Test the center and edges of the claimed operating range, not only the easiest setting. Randomize sample order to reduce learning and fatigue effects. When differences are small, repeat the comparison and examine recorded electrical signals before attributing the result to mineral chemistry.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

23. Analytical Methods for Routine Control

XRF is efficient for major oxides, ICP methods support trace-element work, laser diffraction or sieving controls size, and gravimetric testing controls moisture. Microscopy, XRD and magnetic checks provide deeper investigation when routine numbers do not explain performance.

Document sample preparation because grinding, splitting and fusion methods strongly affect mineral results. Use reference materials, duplicates and periodic external proficiency checks. Supplier and buyer results should be compared by method before either side declares that the other laboratory is wrong.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

24. Incoming Sampling and Lot Release

A certificate represents the supplier’s sample, while the buyer receives many bags or a bulk container. Sampling must capture lot variation without contaminating the material. Composite samples, sealed retain samples and traceable labels create the evidence needed for release and investigation.

Define lot size, number of increments, sampling tools and retention period in the quality agreement. Release critical lots only after priority tests are complete. Trend TiO2, moisture, key impurities, particle size and bulk density so that shifts are seen before welding complaints appear.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

25. Supplier Qualification and Total Cost

A capable supplier controls ore source, beneficiation, milling, magnets, screens, packaging and change notification. Qualification should examine process consistency, laboratory capability, traceability, capacity and corrective-action discipline, not only a polished certificate.

Calculate total cost through usable yield, line rate, drying losses, electrode rejection, welding productivity and complaint risk. Approve a source after repeated lots and a production-scale trial. Maintain an alternate source with the same evidence so that supply resilience does not depend on emergency substitutions.

For qualification, convert this factor into a written test method, sampling rule and acceptance decision. Review at least three representative lots, preserve raw data and compare results with the approved control. When a value moves within specification but process behavior changes, investigate the trend instead of assuming the limit is sufficient. This discipline protects formulation knowledge, reduces emergency adjustments and gives the supplier a precise basis for corrective action.

Frequently Asked Questions

Is higher TiO2 always better in rutile sand?

No. A higher assay can be useful, but particle size, mineral phases and impurities determine actual welding performance. The best grade is the one validated in the complete formula.

Can pigment-grade TiO2 replace rutile sand directly?

Usually not without reformulation. Pigment TiO2 has different particle size, surface treatment and economics, so direct substitution can change mixing, slag and arc behavior.

Which particle-size value should be specified?

Use a distribution appropriate to the process, such as D10, D50 and D90 plus oversize control, with the method and dispersion conditions fixed.

Why can two lots with the same TiO2 weld differently?

They may differ in iron-bearing phases, silica, alumina, trace elements, surface texture, moisture or fine-particle fraction.

How many lots are needed for supplier approval?

There is no universal number, but multiple independent lots and a production-scale trial are far stronger evidence than one handpicked sample.

Should every incoming lot be welding-tested?

Routine release can rely on correlated chemical and physical controls, while periodic welding audits and change-triggered trials confirm that correlations remain valid.

What is the most important supplier document?

The specification and certificate matter, but a change-notification agreement, traceability records and evidence of process control are equally important.

How should a failed lot be investigated?

Quarantine it, verify sampling and methods, compare with the retained approved sample, review manufacturing data and conduct a controlled welding comparison before deciding disposition.

Conclusion

Successful qualification of rutile sand for welding electrode flux combines mineral chemistry, particle control, manufacturing behavior and welding evidence. A specification becomes valuable only when each limit is tied to a stable method and an observed process risk. By using retained controls, repeated lots, disciplined trials and supplier change management, manufacturers can secure consistent arc performance, manageable slag, attractive beads and reliable production economics.

Phenyl silicone oil samples with viscosity and high-temperature laboratory testing equipment

Phenyl Silicone Oil for High-Temperature Applications: Thermal Stability, Viscosity, Volatility Testing and Supplier Qualification

Phenyl silicone oil for high-temperature applications combines the flexible siloxane backbone with phenyl groups that modify heat resistance, low-temperature behavior, refractive index and compatibility. It is used where ordinary silicone fluids or hydrocarbon oils may not provide the required operating range.

This guide explains how to compare phenyl content, viscosity, thermal stability, volatility and material compatibility; how to design laboratory and pilot trials; and how to qualify a supplier. Selection must be based on the complete duty cycle rather than one attractive data-sheet value.

1. Molecular structure and phenyl modification

Molecular structure and phenyl modification should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

2. Phenyl content and property balance

Phenyl content and property balance should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

3. Thermal stability in air and inert service

Thermal stability in air and inert service should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

4. Oxidation resistance and aging behavior

Oxidation resistance and aging behavior should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

5. Low-temperature fluidity

Low-temperature fluidity should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

6. Viscosity grade selection

Viscosity grade selection should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

7. Viscosity-temperature relationship

Viscosity-temperature relationship should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

8. Flash point and fire-safety review

Flash point and fire-safety review should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

Thermal stability and volatility testing of phenyl silicone oil in an industrial laboratory
Controlled thermal aging connects mass loss, viscosity and color change.

9. Volatility and evaporation loss

Volatility and evaporation loss should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

10. Color and clarity

Color and clarity should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

11. Refractive index as an identity check

Refractive index as an identity check should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

12. Density and batch consistency

Density and batch consistency should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

13. Compatibility with metals

Compatibility with metals should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

14. Compatibility with elastomers and seals

Compatibility with elastomers and seals should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

15. Compatibility with organic fluids

Compatibility with organic fluids should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

16. Heat-transfer applications

Heat-transfer applications should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

Phenyl silicone oil high-temperature circulation and heat-transfer pilot trial
A pilot circulation trial verifies pumping, temperature control and material compatibility.

17. High-temperature lubrication

High-temperature lubrication should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

18. Electrical and dielectric uses

Electrical and dielectric uses should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

19. Vacuum and low-pressure service

Vacuum and low-pressure service should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

20. Foaming and air release

Foaming and air release should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

21. Moisture and contamination control

Moisture and contamination control should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

22. Laboratory thermal-aging test

Laboratory thermal-aging test should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

23. Pilot circulation trial

Pilot circulation trial should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

24. Quality-control specification

Quality-control specification should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

25. Supplier qualification and total cost

Supplier qualification and total cost should be evaluated against the exact operating temperature, atmosphere, residence time and equipment materials. Phenyl silicone fluids with different composition and viscosity can behave differently in oxidation, evaporation, pumping, seal contact and heat transfer. A generic silicone-oil description is not enough for technical approval.

Use a controlled reference and document sample identity, test temperature, duration, surface area, atmosphere and cooling method. Measure viscosity, mass loss, color, acidity, deposits and relevant performance before and after exposure. Multiple time points reveal whether degradation is linear, accelerating or caused by a temporary start-up effect.

Qualification must also connect laboratory results with the production system. Review pumpability, pressure, heat-transfer rate, leakage, foaming, seal condition, metal cleanliness and maintenance requirements. Retain labeled samples and raw records so every result can be traced to the exact lot and test condition.

Frequently Asked Questions

Why add phenyl groups to silicone oil?

The answer depends on composition, viscosity, temperature, atmosphere, duration and equipment materials. Compare candidates through a documented application test, use an approved reference, and confirm laboratory conclusions in a representative pilot or production system.

Which viscosity grade should be selected?

The answer depends on composition, viscosity, temperature, atmosphere, duration and equipment materials. Compare candidates through a documented application test, use an approved reference, and confirm laboratory conclusions in a representative pilot or production system.

How should thermal stability be tested?

The answer depends on composition, viscosity, temperature, atmosphere, duration and equipment materials. Compare candidates through a documented application test, use an approved reference, and confirm laboratory conclusions in a representative pilot or production system.

Does phenyl silicone oil work at low temperature?

The answer depends on composition, viscosity, temperature, atmosphere, duration and equipment materials. Compare candidates through a documented application test, use an approved reference, and confirm laboratory conclusions in a representative pilot or production system.

How is evaporation loss measured?

The answer depends on composition, viscosity, temperature, atmosphere, duration and equipment materials. Compare candidates through a documented application test, use an approved reference, and confirm laboratory conclusions in a representative pilot or production system.

Can it contact common seals?

The answer depends on composition, viscosity, temperature, atmosphere, duration and equipment materials. Compare candidates through a documented application test, use an approved reference, and confirm laboratory conclusions in a representative pilot or production system.

What incoming tests are useful?

The answer depends on composition, viscosity, temperature, atmosphere, duration and equipment materials. Compare candidates through a documented application test, use an approved reference, and confirm laboratory conclusions in a representative pilot or production system.

What should a supplier provide?

The answer depends on composition, viscosity, temperature, atmosphere, duration and equipment materials. Compare candidates through a documented application test, use an approved reference, and confirm laboratory conclusions in a representative pilot or production system.

Conclusion

Phenyl silicone oil can provide a broad temperature range, controlled viscosity and useful thermal performance when its composition is matched to the application. Approval should combine aging, volatility, compatibility and circulation data with a clear quality specification.

Hengyi Technology supports sample selection and application-focused qualification for phenyl silicone oil. Visit Hengyi Technology for related silicone-fluid resources.